Workpiece-led production planning
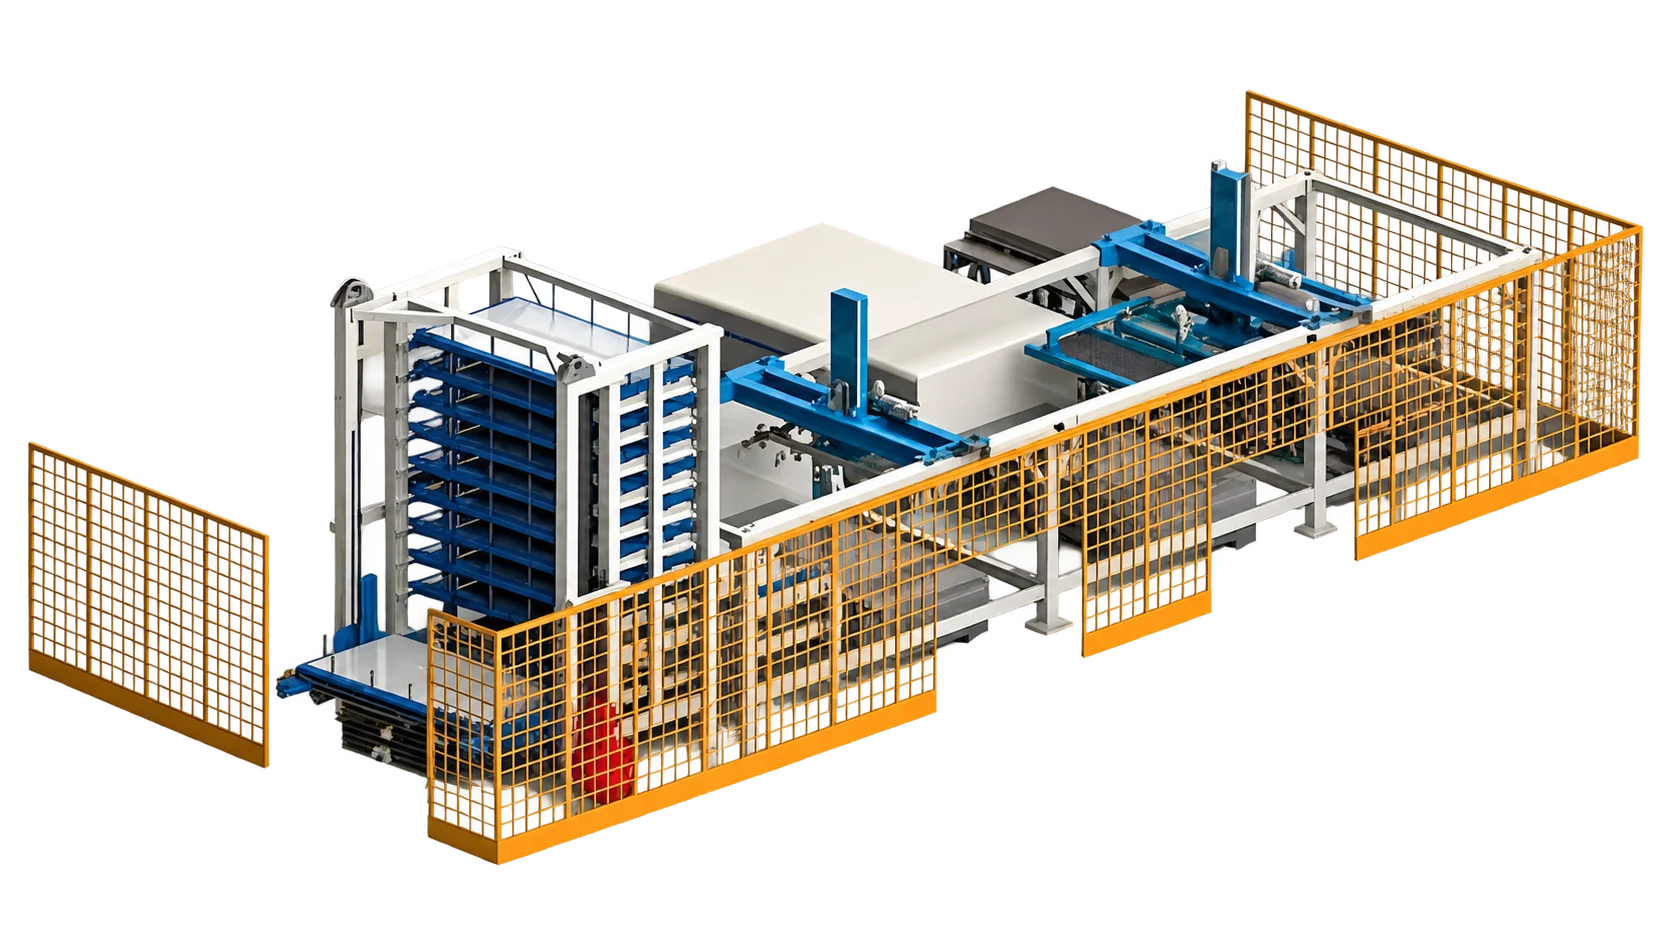
Complete basket-production solution
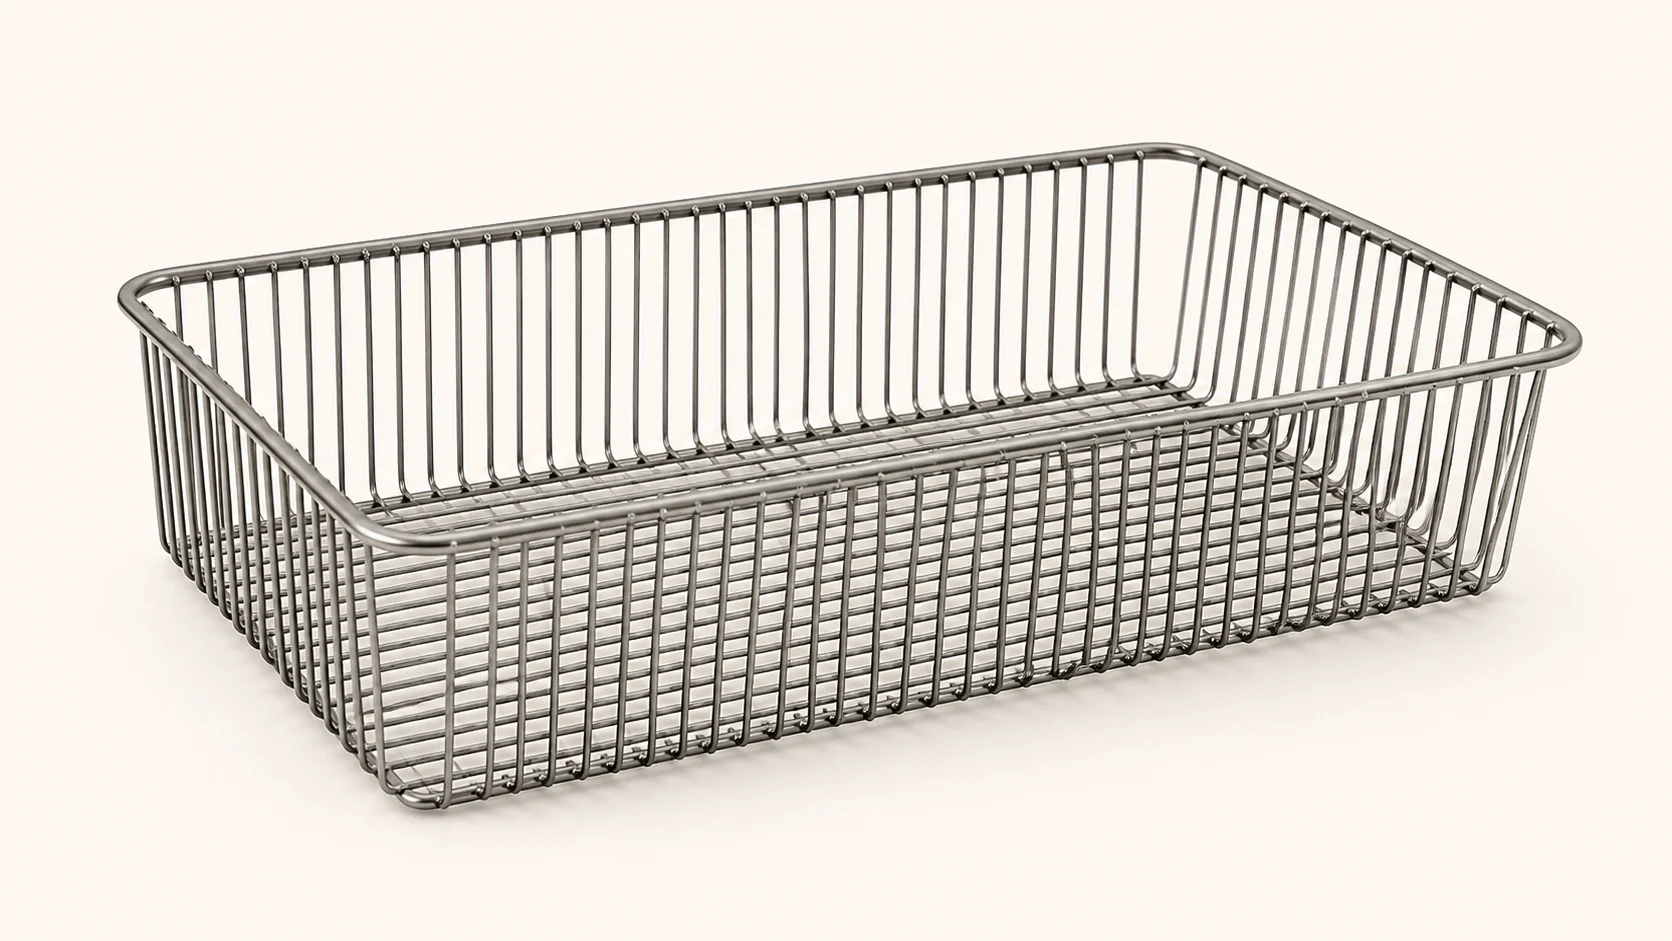
Configure equipment for manufacturing wire baskets from your part drawing and production requirements. Choose a 2D wire-forming, 3D wire-forming or welded-mesh route, then define the stations, fixtures and handoffs needed for that basket.
Entry routes3routes
Mapped stages8stages
Planning basisPartdrawing
The equipment combination, fixtures, automation boundary and process sequence are confirmed after the basket drawing and production target are reviewed.
Specifications
Basket solution configuration
Solution configuration
- Entry routes
- 2D wire forming / 3D wire forming / welded mesh
- Preparation
- Straightening, shearing and high-speed straightening as required
- Forming and trimming
- Folding, butt welding, trimming and hydraulic forming as required
- Assembly welding
- Spot welding, row welding and fixture-based assembly operations
- Completion
- Inspection, weld reinforcement, surface-treatment coordination and packing
- Configuration basis
- Basket drawing, sample, material, wire size, joint design and output target
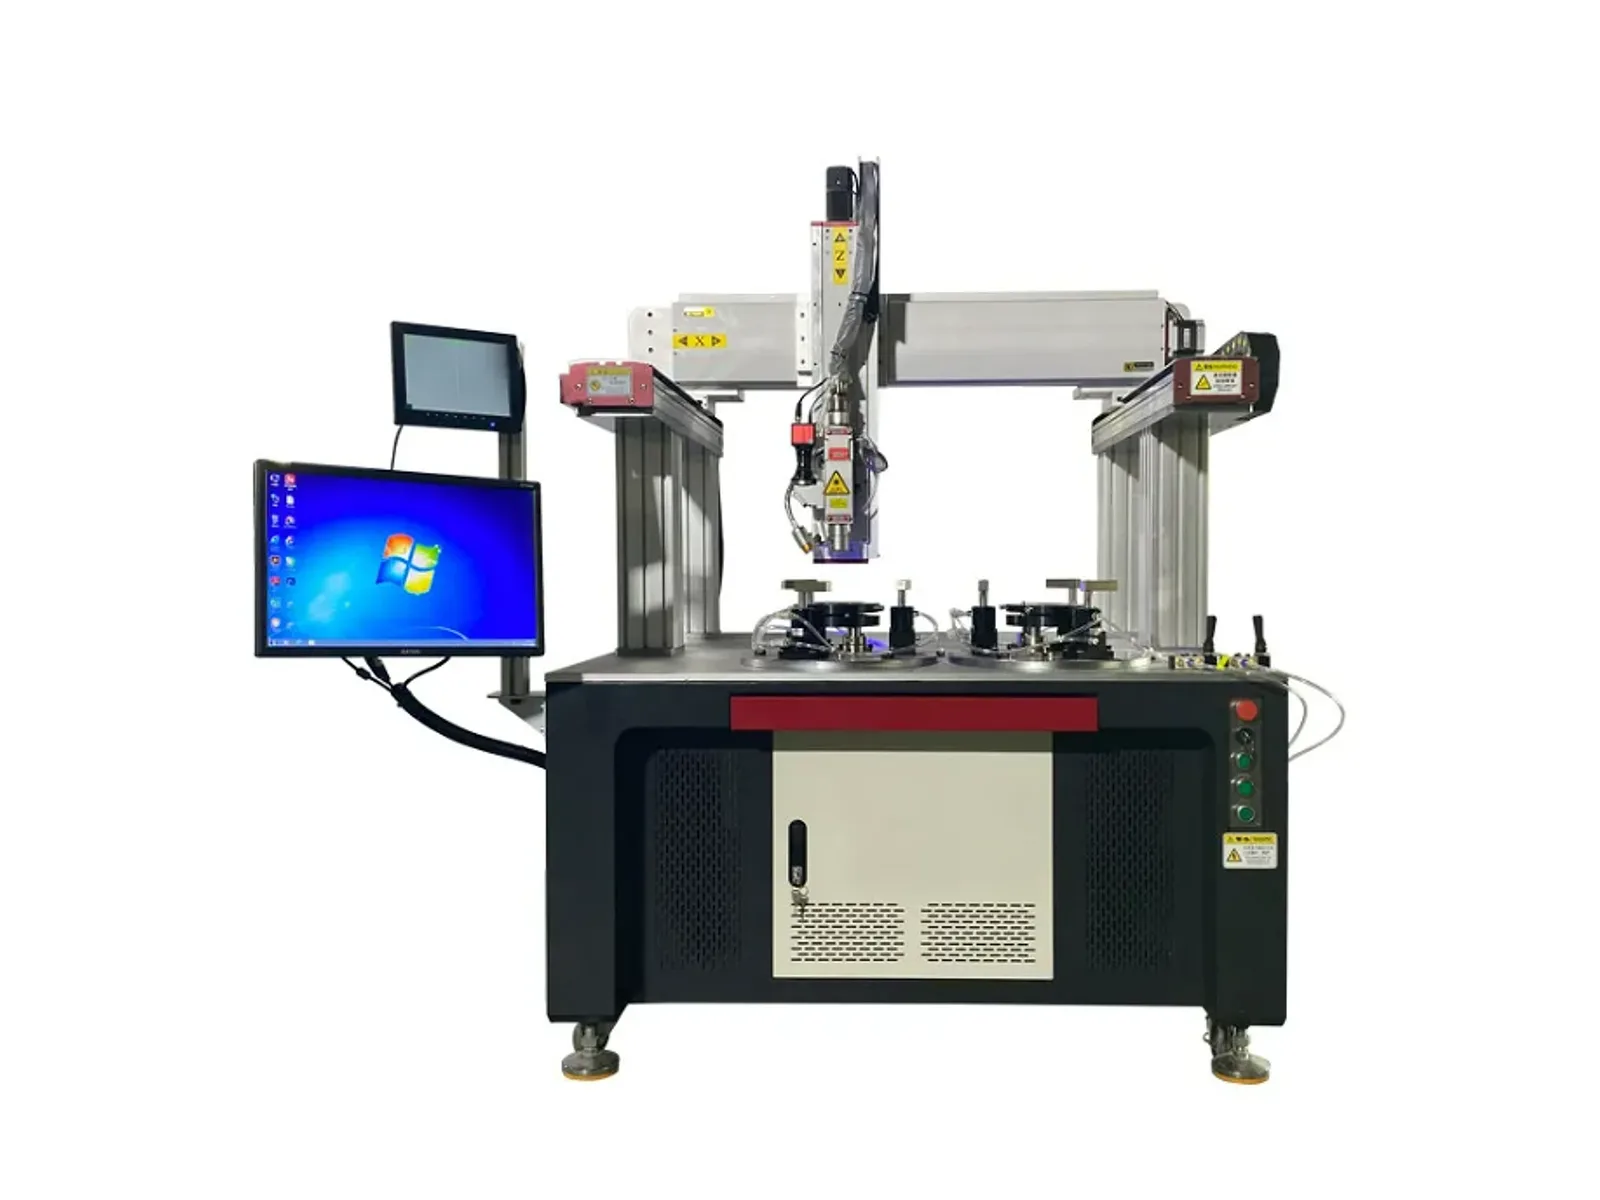
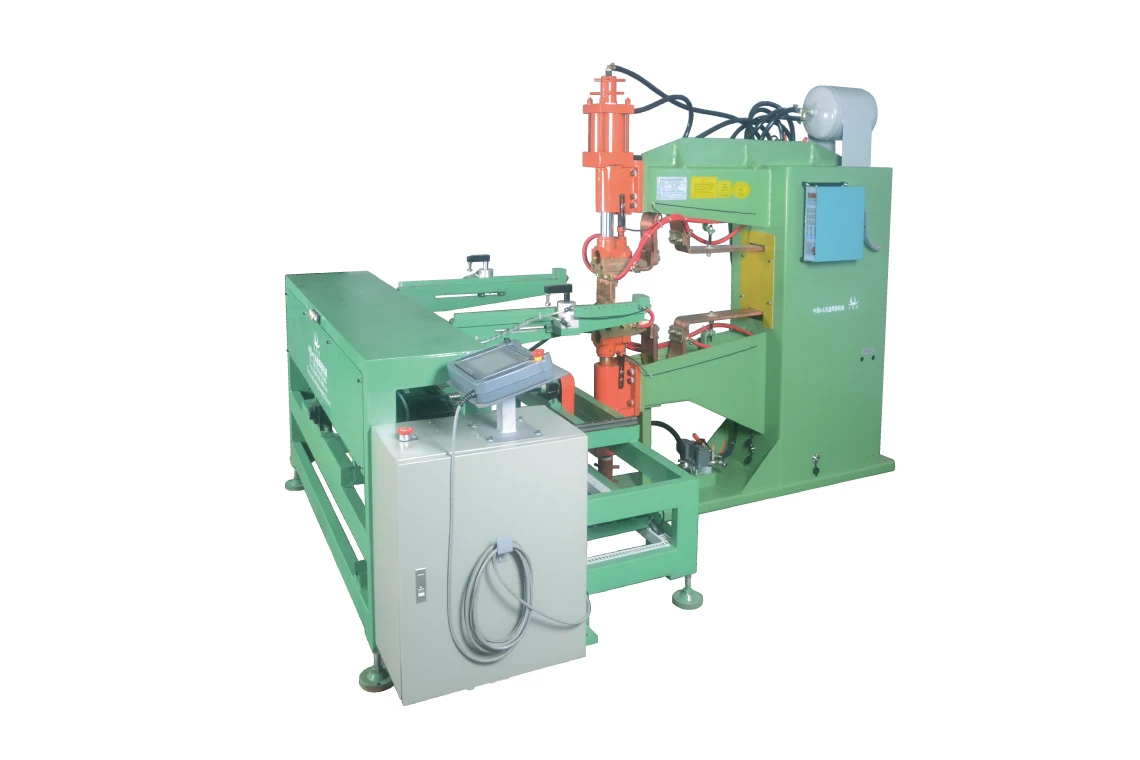
XY-axis automatic row welding station
- Equipment
- XY-axis automatic row welding machine
- Motion
- Servo-driven X/Y mold-frame movement controlled by the system
- Programs
- Multiple product specifications can be stored in the controller
- Operation
- Programmed welding sequence with return to origin; foot-switch start is listed
- Configuration scope
- Station capabilities are selected according to the configured production line
Features
Capabilities of the XY-axis row-welding station
The XY-axis automatic row welder is one configurable station inside the basket workflow. These capabilities apply to that station, not automatically to every equipment combination.
01
Servo-controlled movement
The X/Y mold frame is driven by a servo motor, with walking step and speed controlled through the control system.
02
Automatic welding sequence
After the workpiece is fixed to the mold frame, the programmed X/Y movement completes the configured weld positions and returns to the origin.
03
Multiple stored programs
The controller can store multiple product specifications, with walking distance and welding sequence set around the workpiece process.
04
Foot-switch start option
The station can also be started by foot switch to support the defined operator workflow and reduce unintended operation.
Production flow
From material preparation to packed basket
The exact route is selected from the stages required for the workpiece.
- 01
Material preparation
- 02
2D / 3D forming or mesh welding
- 03
Forming and trimming
- 04
Basket-body assembly
- 05
Inspection
- 06
Weld reinforcement
- 07
Surface treatment
- 08
Packing
Process routes
Three ways to enter the basket workflow
The drawing determines which route is used and which downstream operations are included.
2D wire-forming routeCreate the primary flat wire geometry before downstream joining and forming.
3D wire-forming routeCombine 3D forming with mechanical handling and butt welding where the geometry requires it.
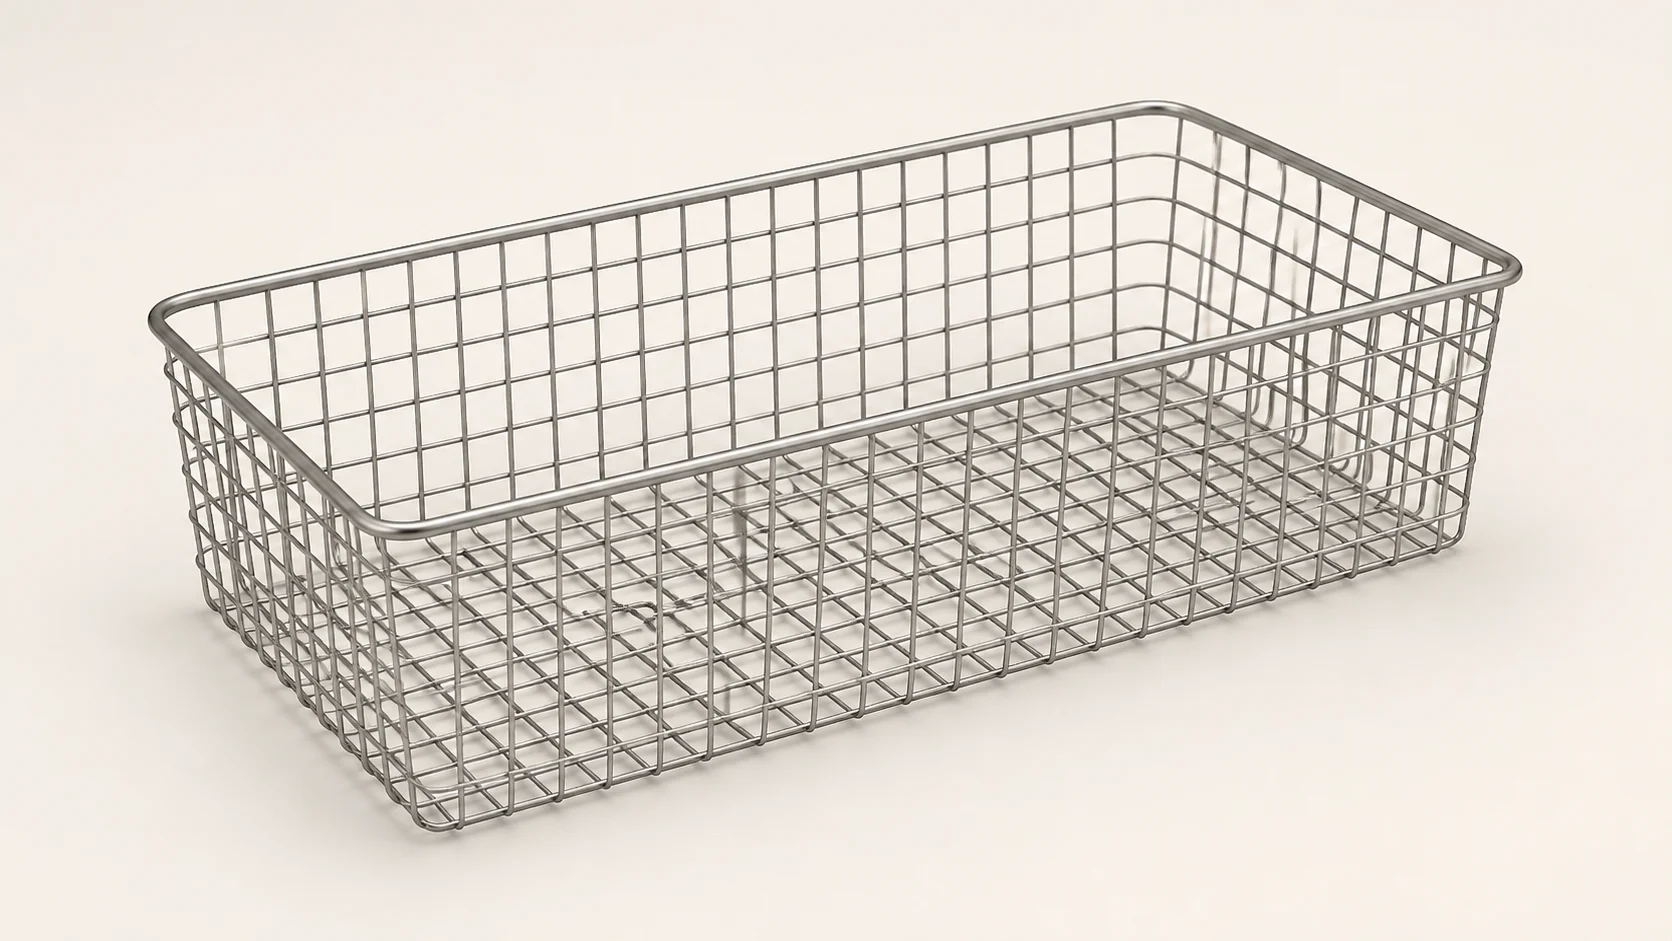
Welded-mesh routeStart with straightening, shearing and automatic mesh row welding before the mesh is formed.
Applications
Basket constructions planned around the workpiece
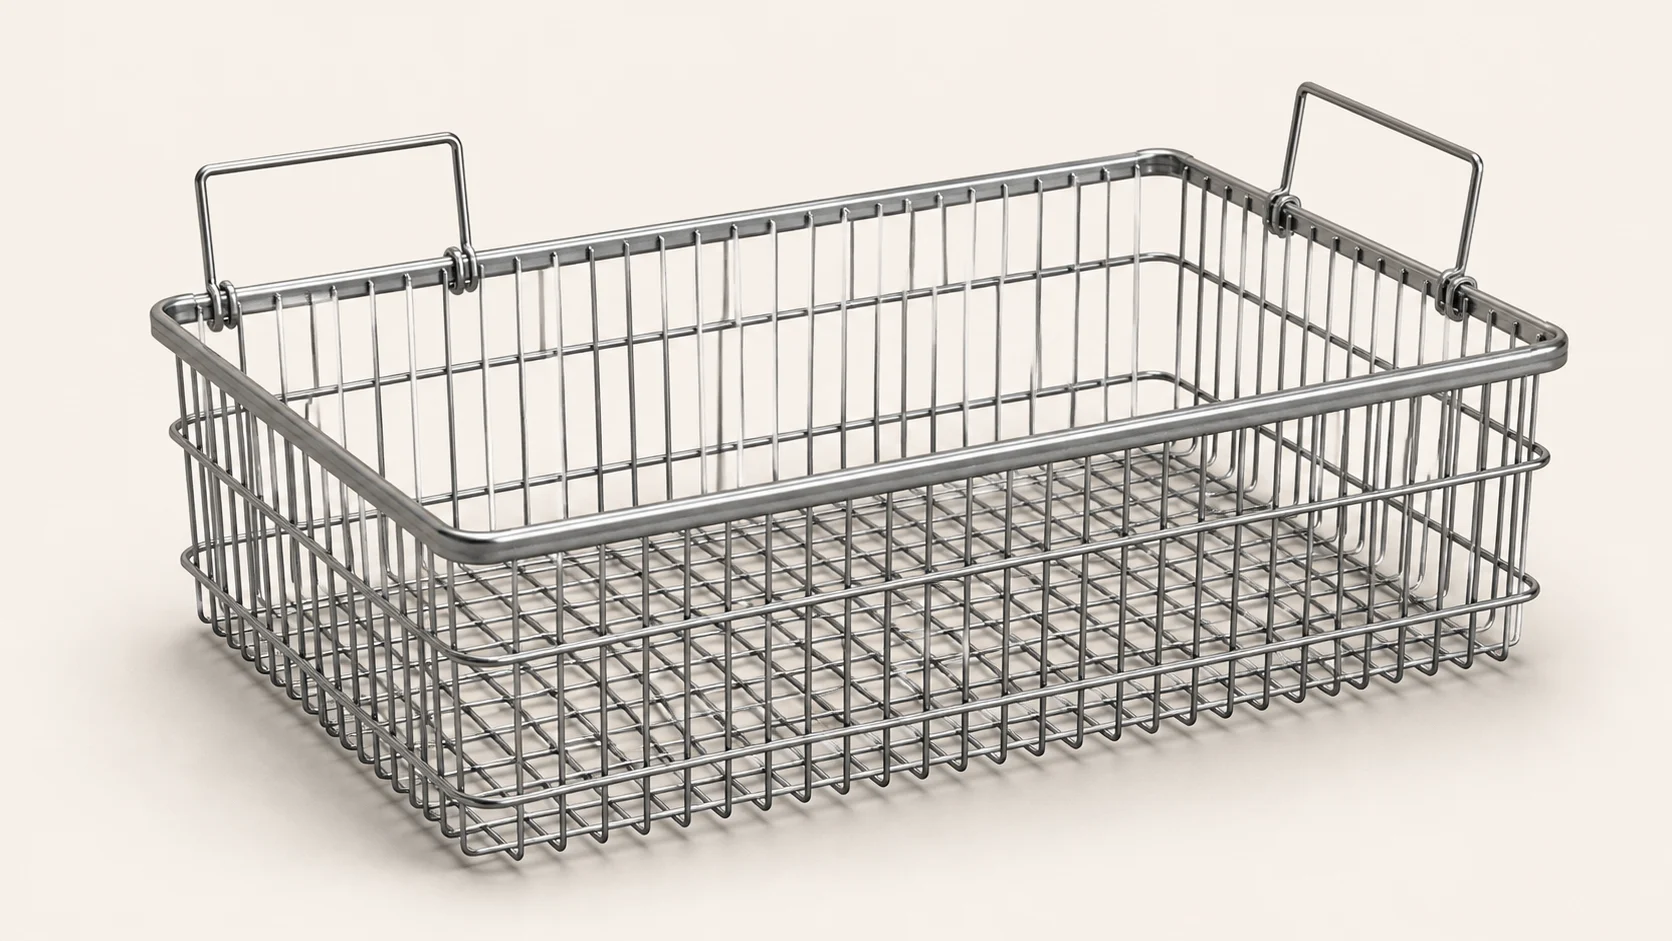
- 04PreparationStraightening, shearing and high-speed straightening
- 05Forming and trimmingFolding, butt welding, trimming and hydraulic forming
- 06Assembly weldingSpot welding, row welding and related fixture-based assembly operations
- 07CompletionInspection, weld reinforcement, surface treatment coordination and packing
Related products
Adjacent automation capabilities
Automation range
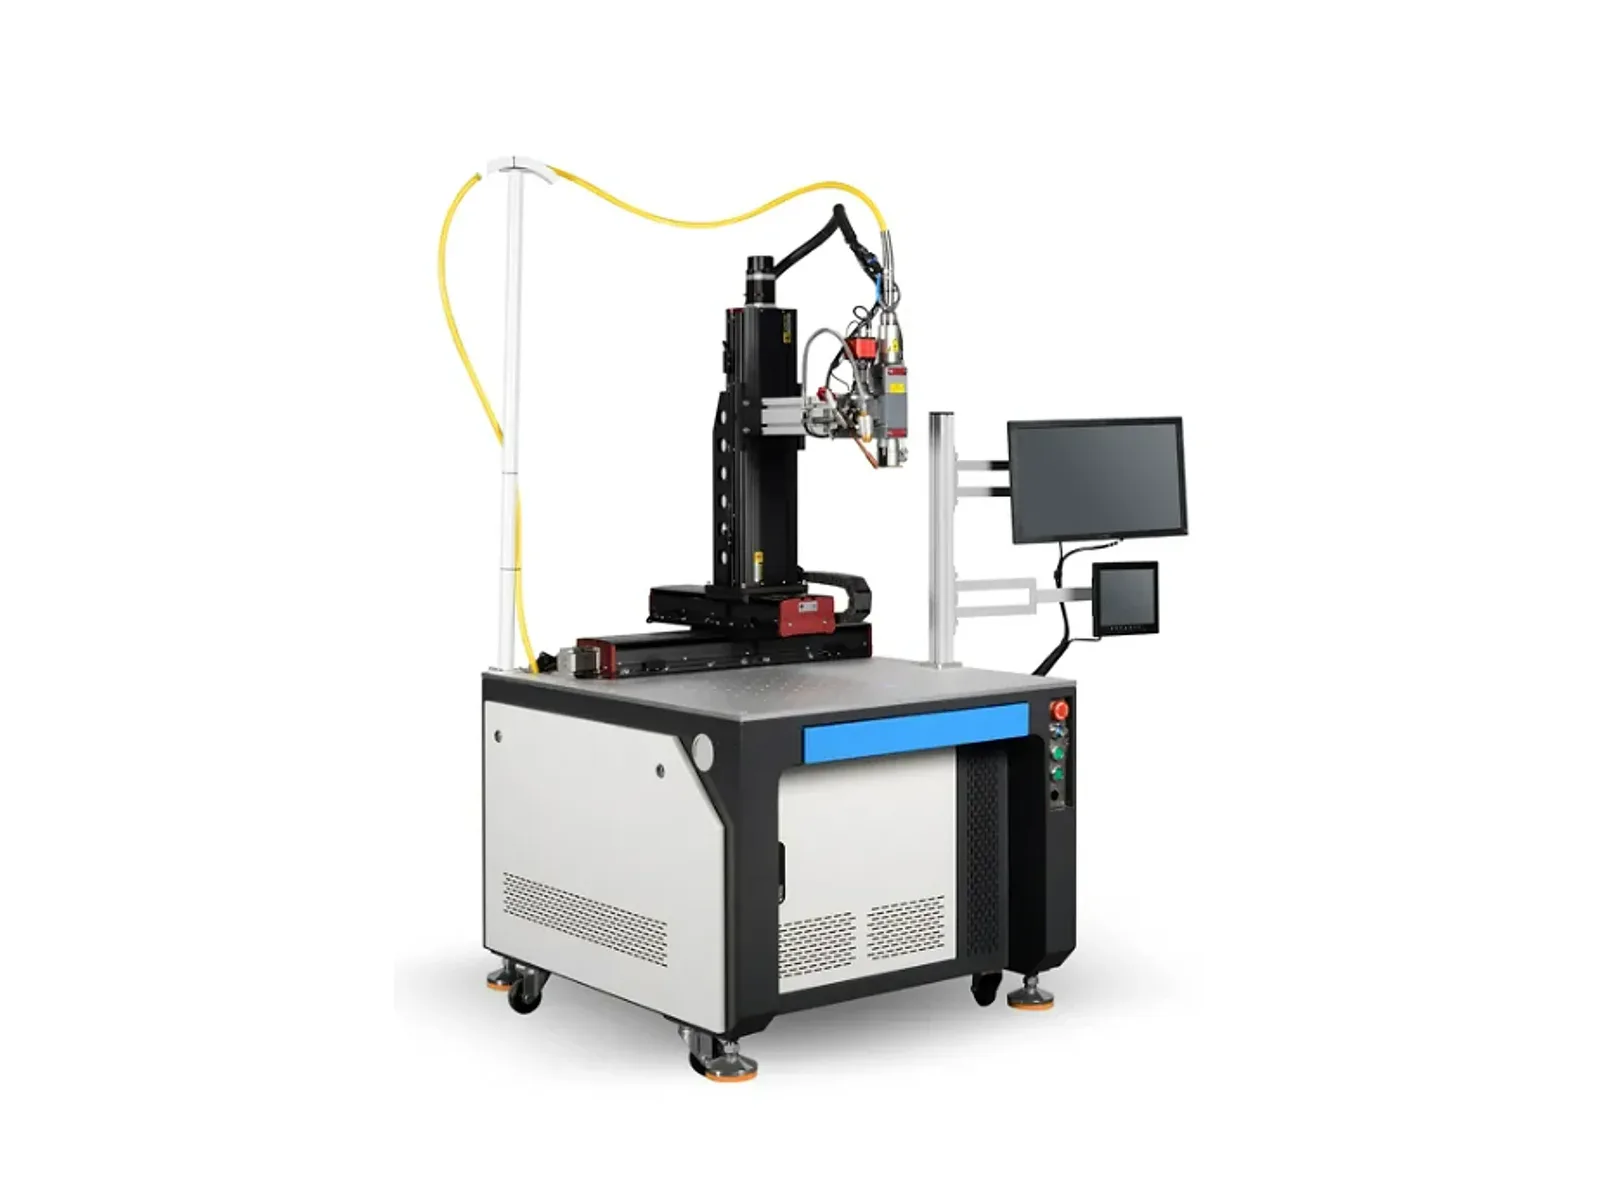
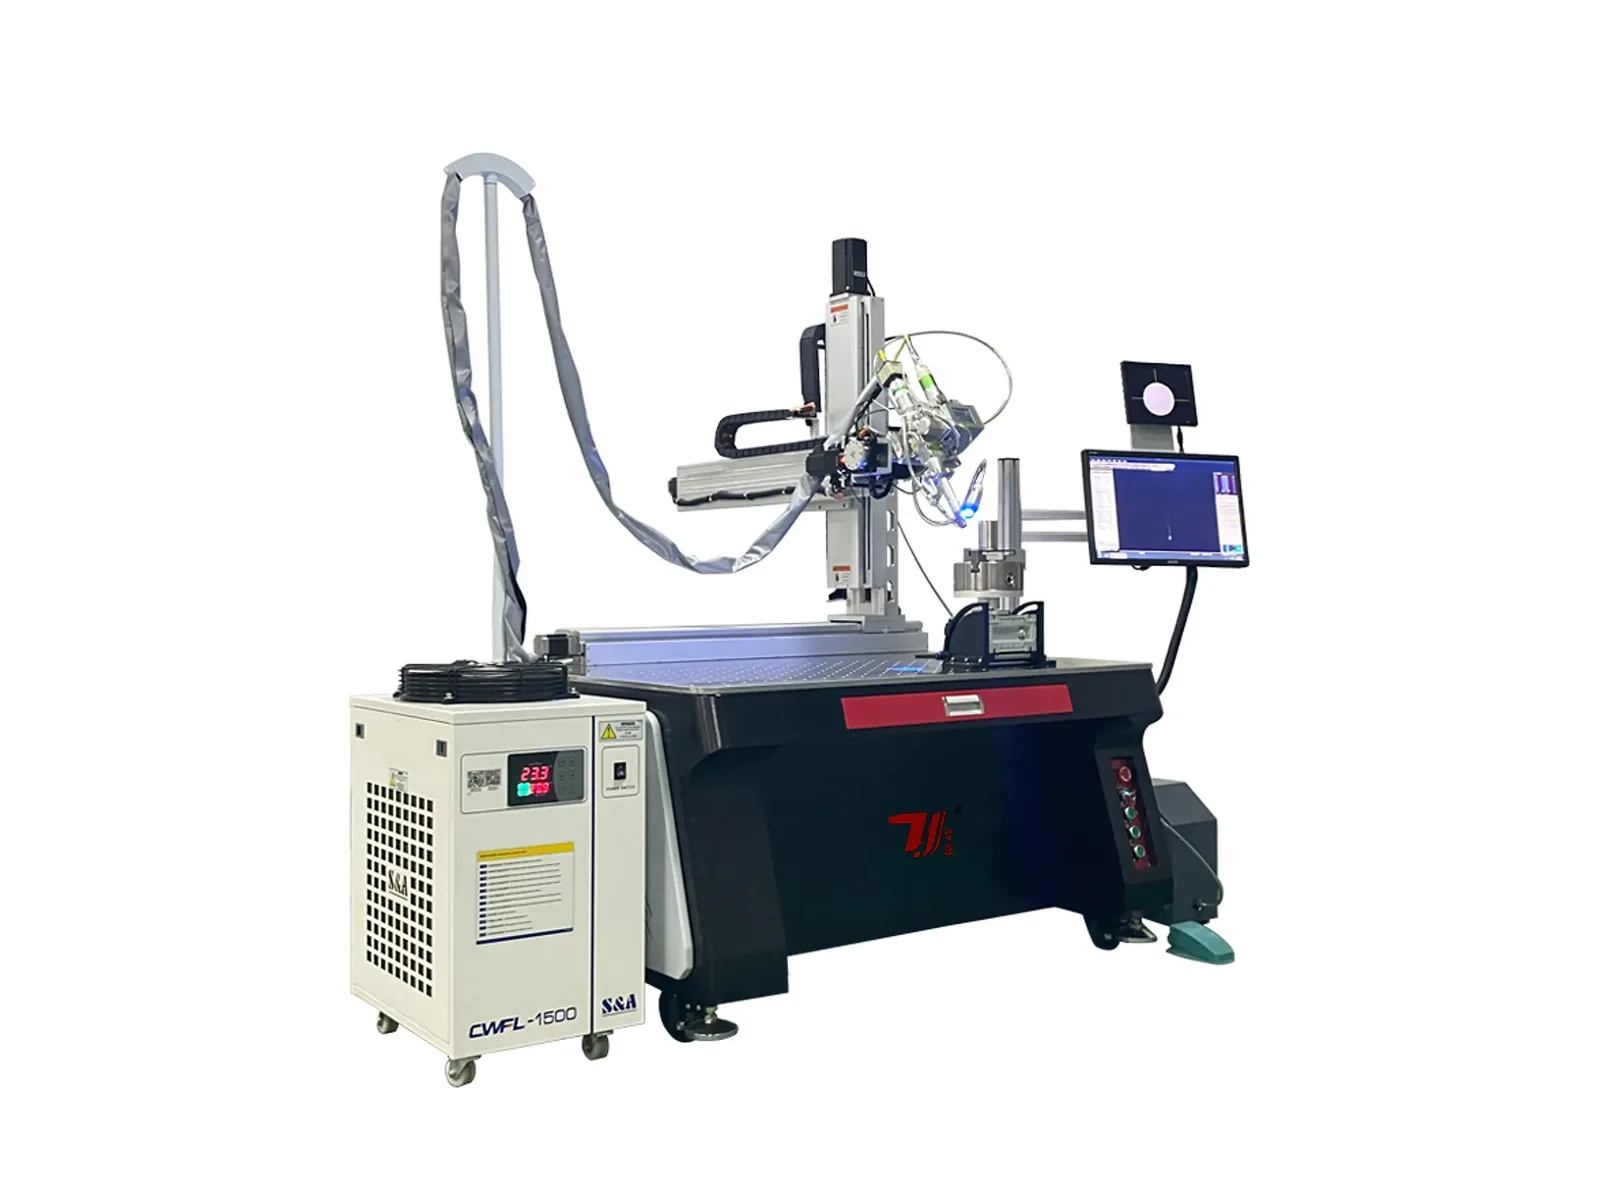
Automatic laser welding
Application-specific welding systems configured around seam geometry and workholding.
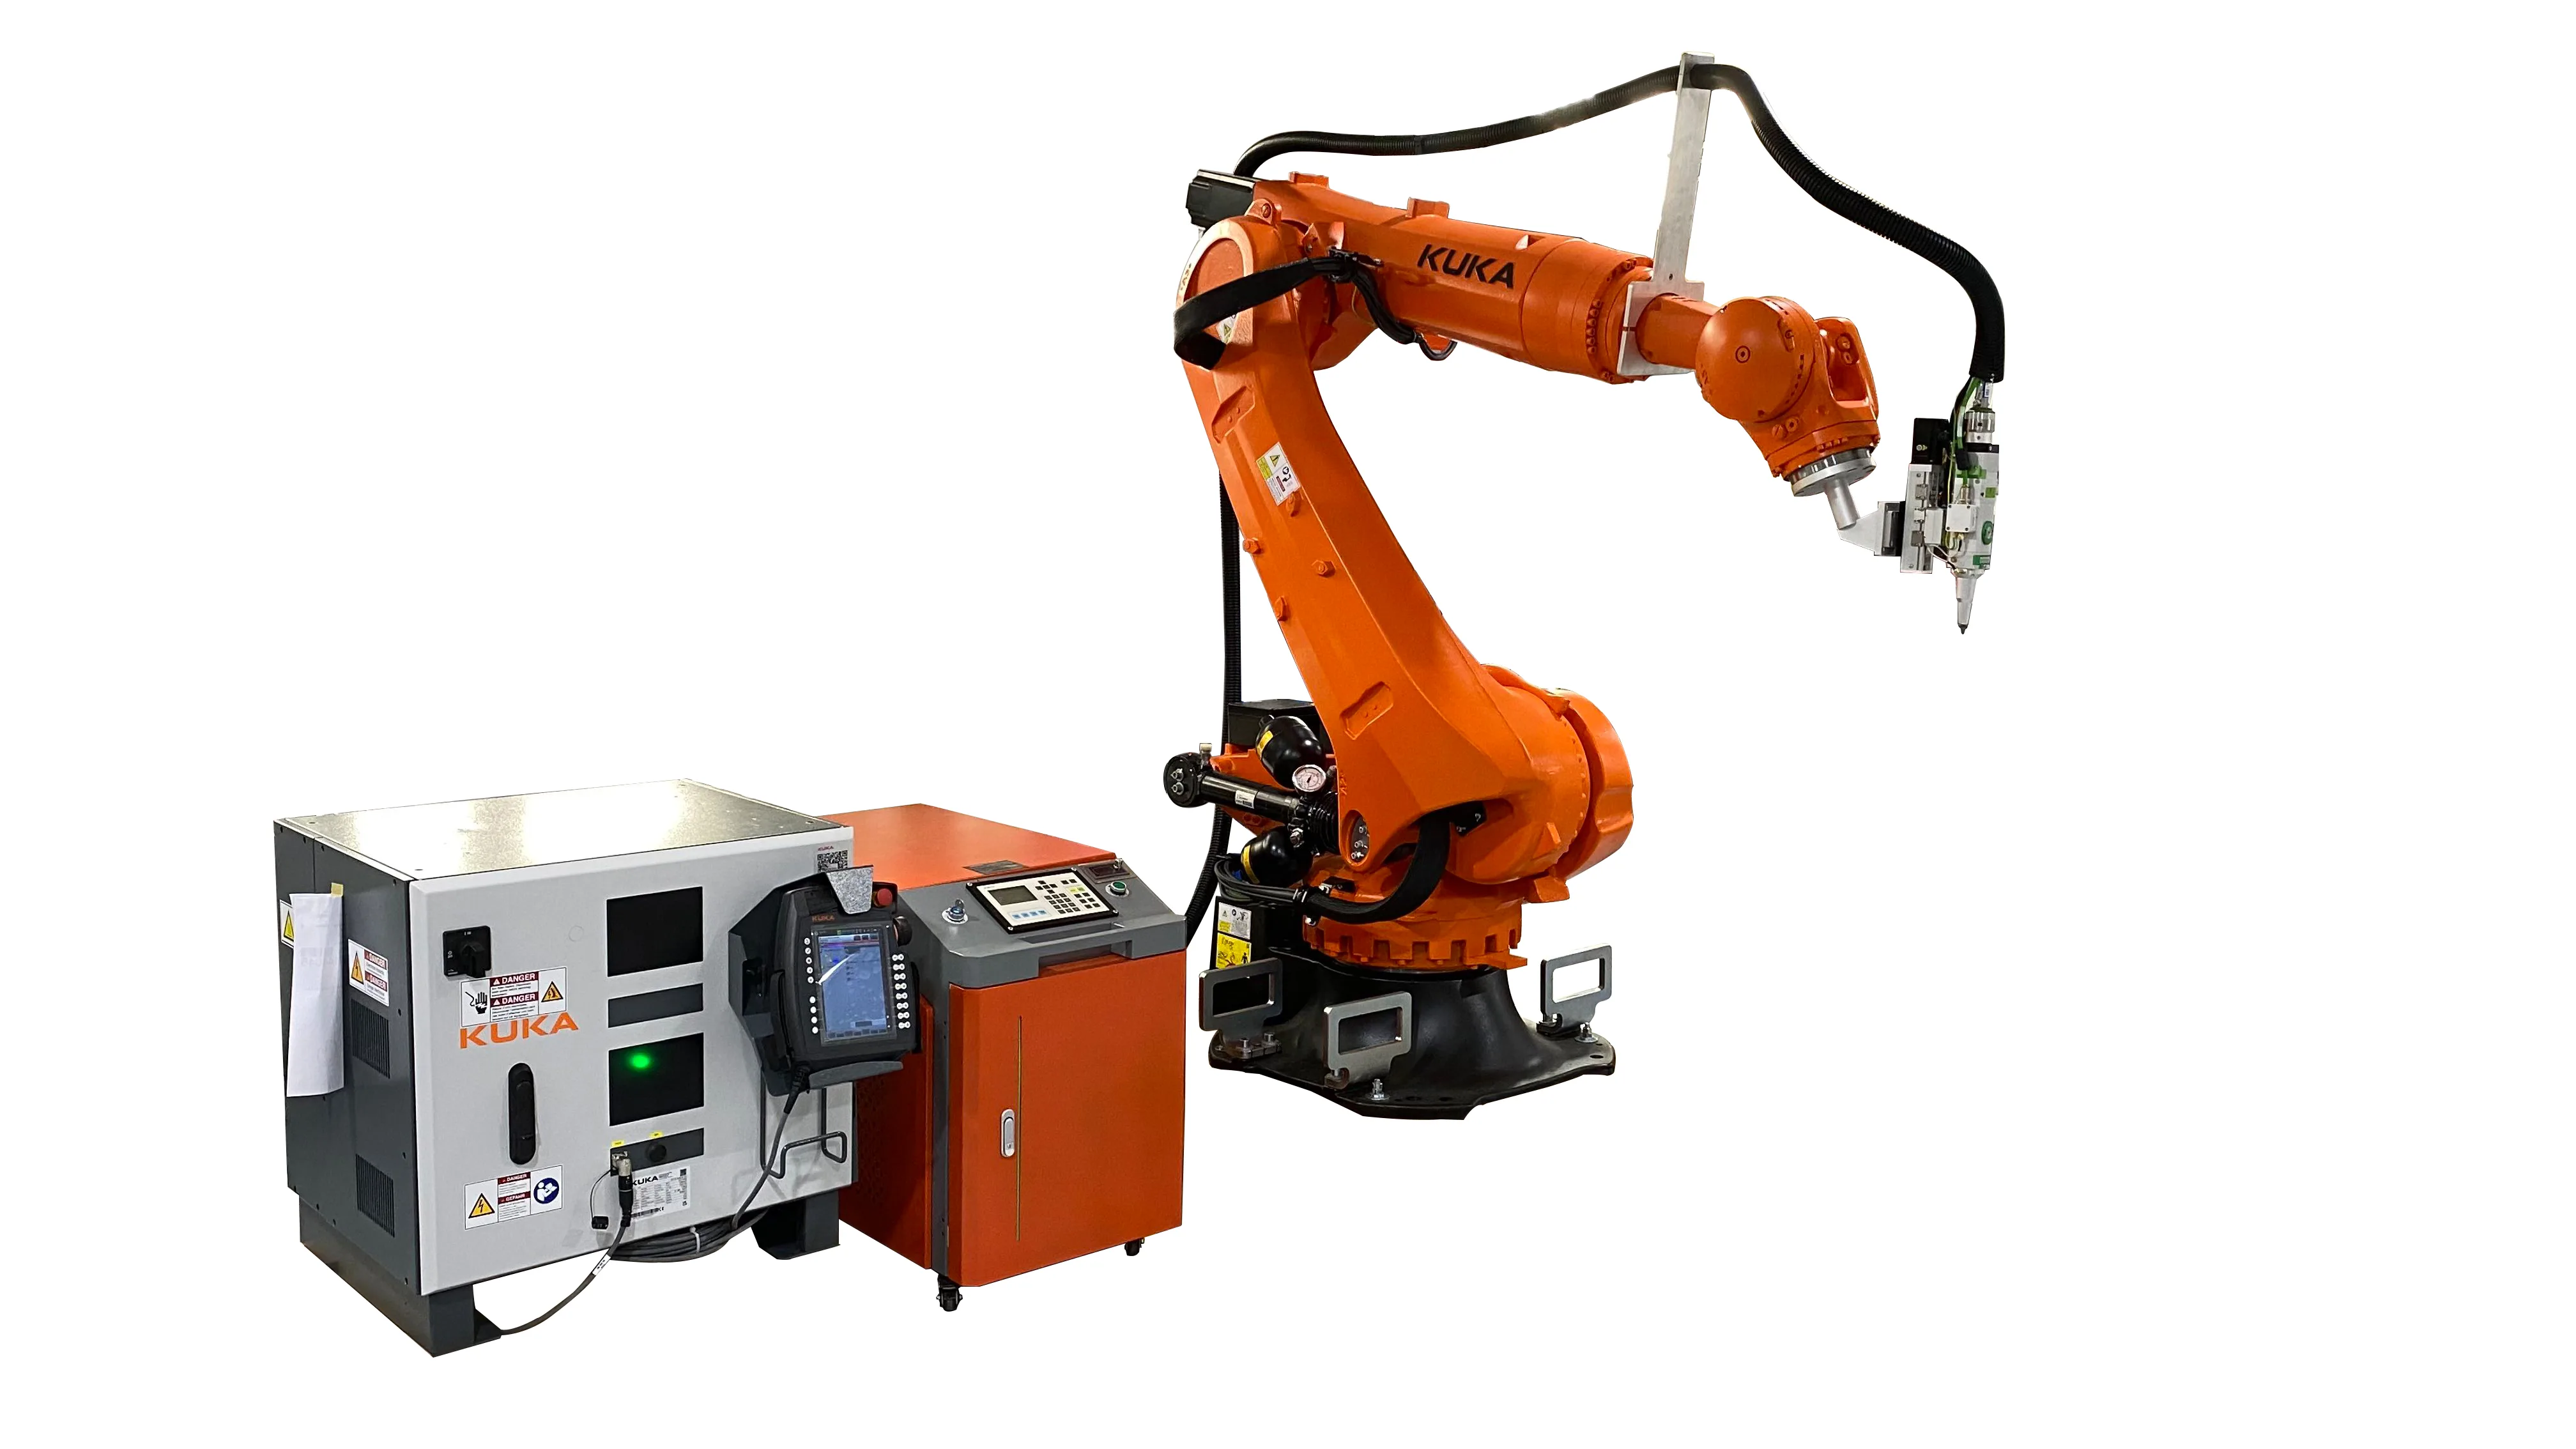
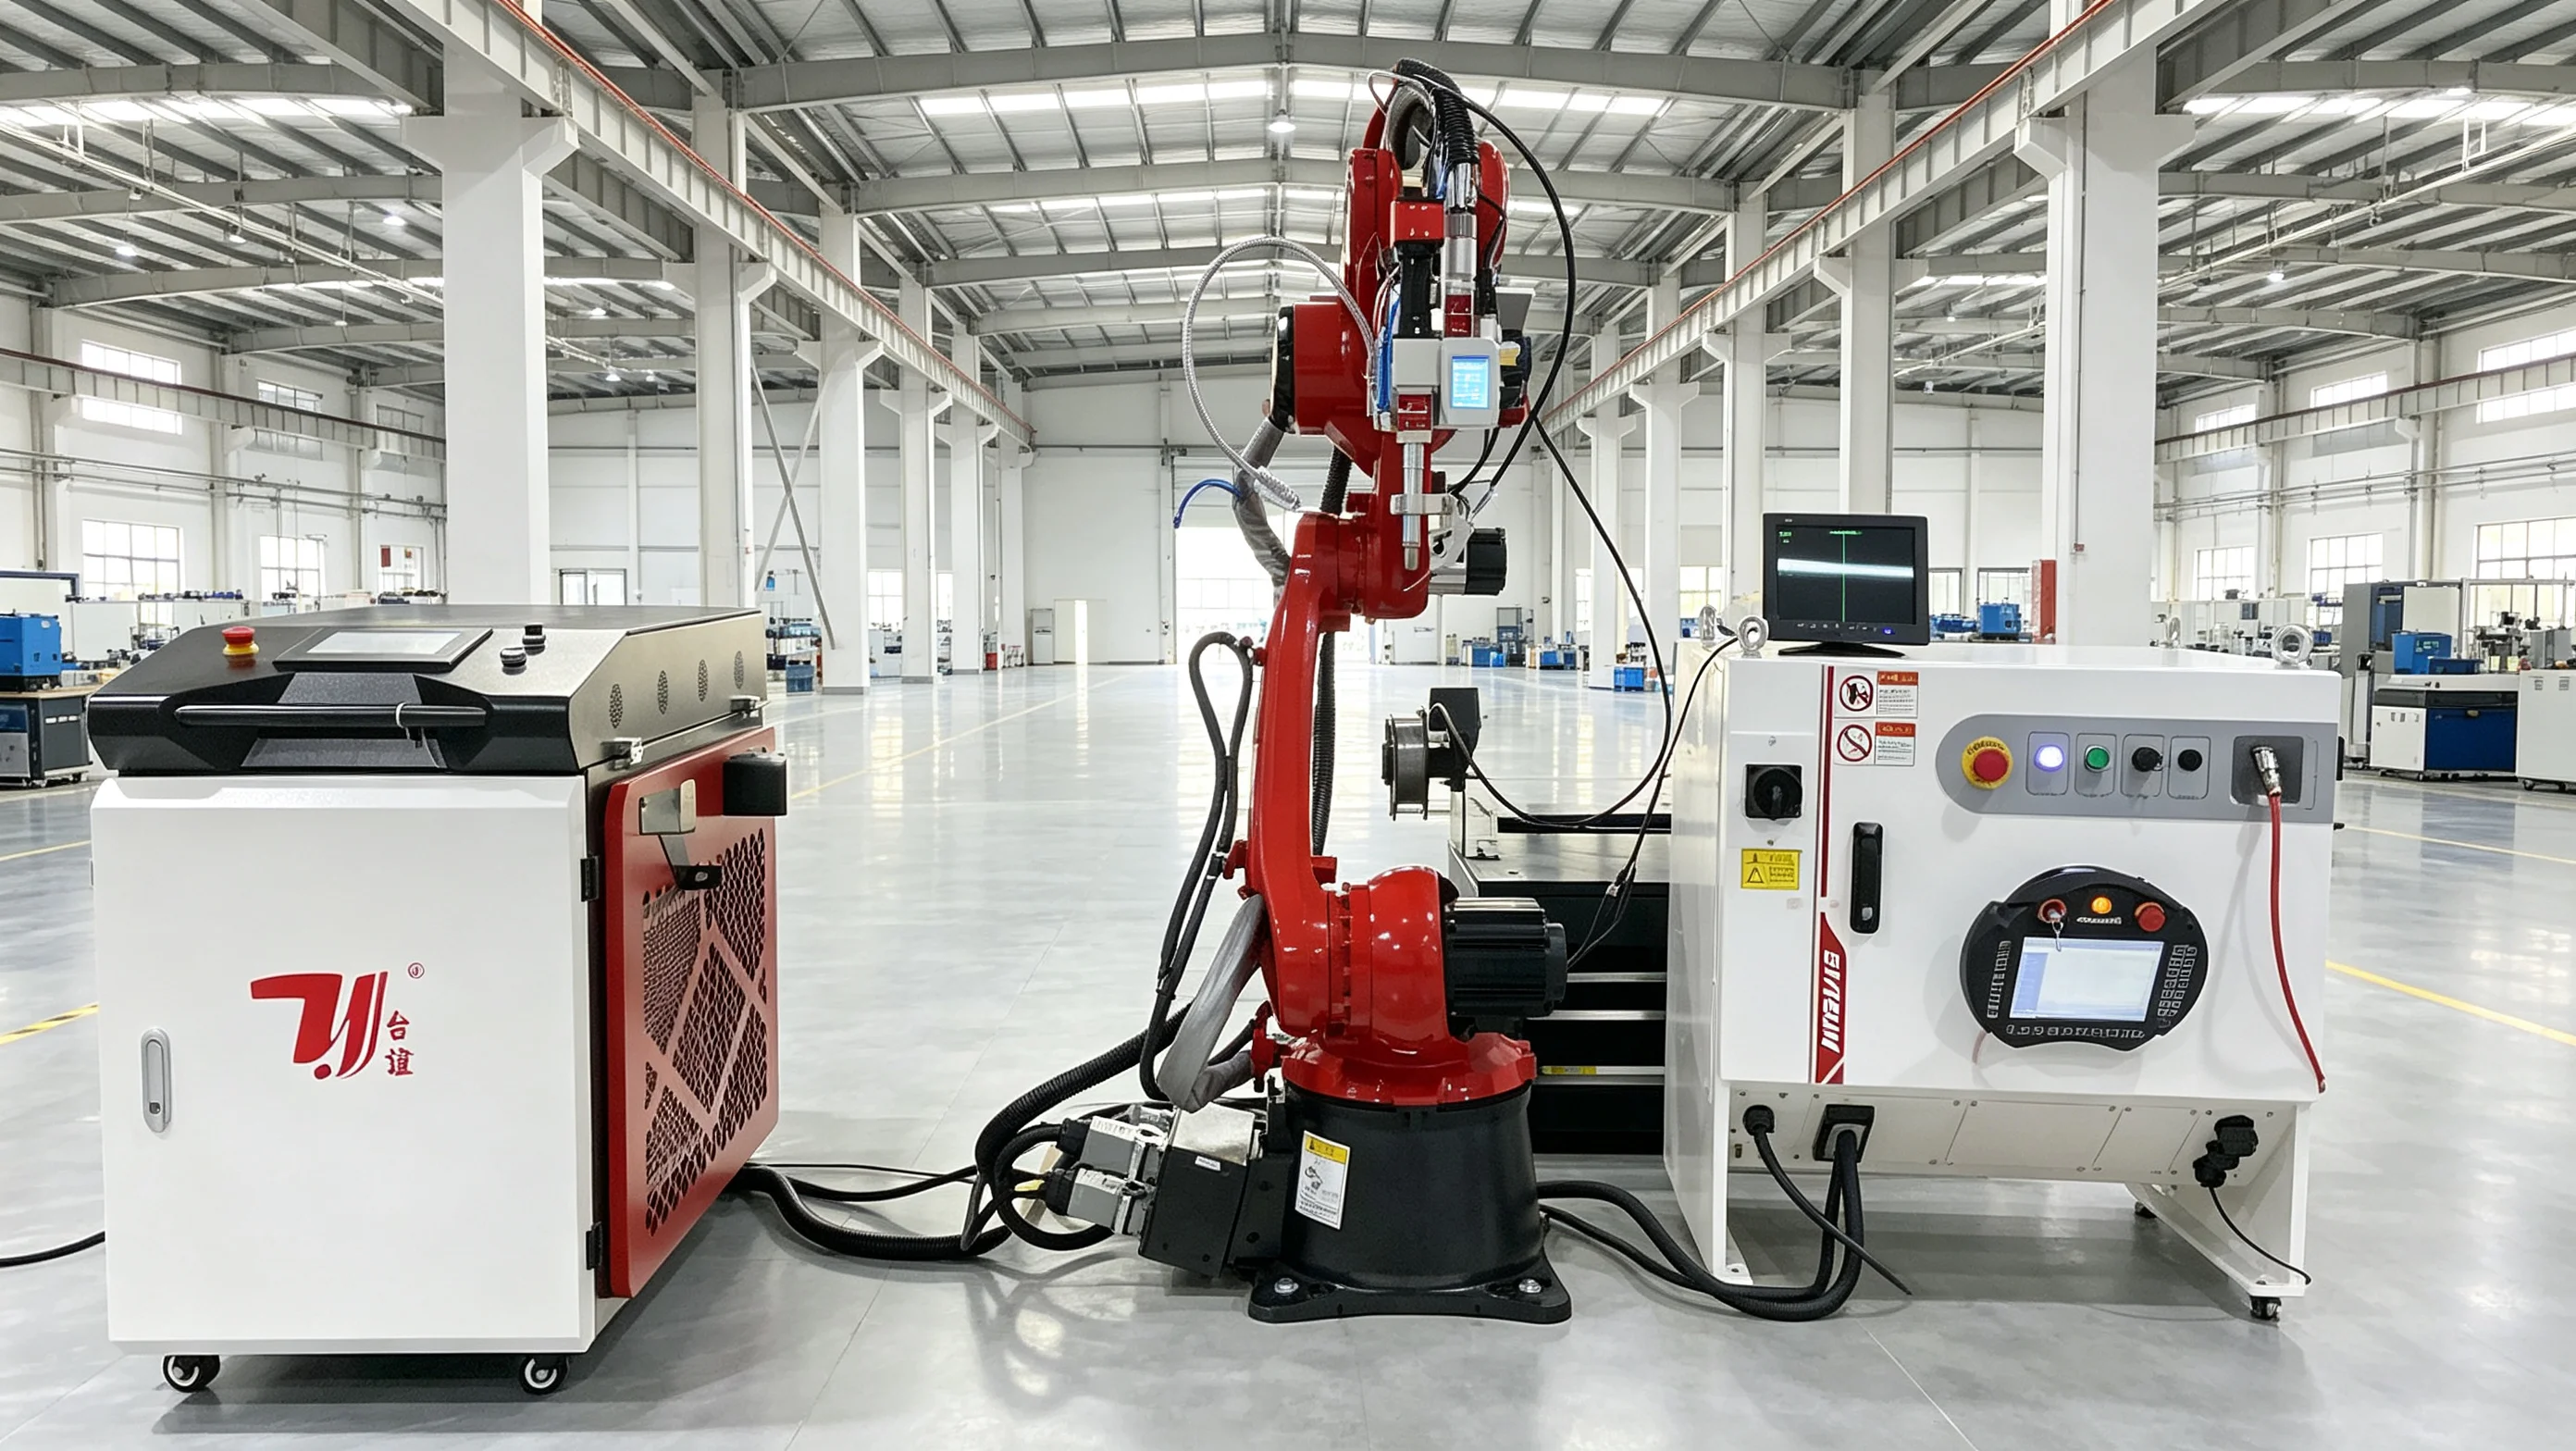
Automation rangeRobot automation systems
Robot processing and material-handling cells for integrated production tasks.
Automation rangeSmart factory systems
Connected loading, cutting and material-storage systems for sheet-metal production.
Explore industry solutions
Browse our industry solutions and discuss the equipment, fixtures and process requirements for your application.
View all industry solutionsDefine the equipment and process boundaries
Select a route from the basket construction
Provide the wire material and diameter, incoming stock form, dimensions and joint locations. Use those inputs to decide which forming, preparation, welding and trimming stages belong in the solution; the three entry routes are alternatives within one configurable offering.
Separate station automation from line automation
The XY row-welding station performs its programmed weld sequence after the workpiece is fixed to the mold frame. Loading, unloading, transfer between stations and changeover require their own defined arrangements; the station sequence does not establish an unattended production line.
Agree the handoff after welding
Specify inspection, reinforcement, surface treatment and packing requirements with the responsible party for each stage. Surface-treatment coordination is not confirmation that coating equipment is included. Agree the supply and acceptance boundary before comparing project quotations.
Machine selection questions
Is this a fixed machine package?
No. It is one configurable basket-production solution. The drawing and process requirements determine the stations and interfaces; not every project requires every stage shown in the pathway.
How are the 2D, 3D and welded-mesh routes selected?
Review the basket geometry, incoming wire or mesh, joint locations and required forming sequence. The routes describe process starting points, not three separate finished-machine models.
What does the XY row-welding station automate?
After the part is fixed to the mold frame, servo-controlled X/Y movement follows the programmed weld positions and returns to the origin. Part loading, unloading and transfer to other stations need a separately agreed scope.
Are surface-treatment machines included?
The workflow includes coordination of the finishing handoff, but this does not confirm coating or other surface-treatment equipment in the supply. Define the process, equipment and responsibility during the engineering review.
What is needed to define output, layout and price?
Send drawings or a sample, wire material and diameter, weld and appearance requirements, target output and loading preferences. Include the factory layout and existing equipment interfaces so fixtures, station sequence, handling and acceptance can be specified.
Request a quote
Tell us the part. We will tell you the machine.
Configuration and quotation are prepared after the basket drawing, process route, automation boundary and production target are reviewed.
- Phone+86 153 6281 4831
- Emailsales02@taiyilaser.com
- WhatsApp+86 153 6281 4831