Dedicated sink-clamp welding
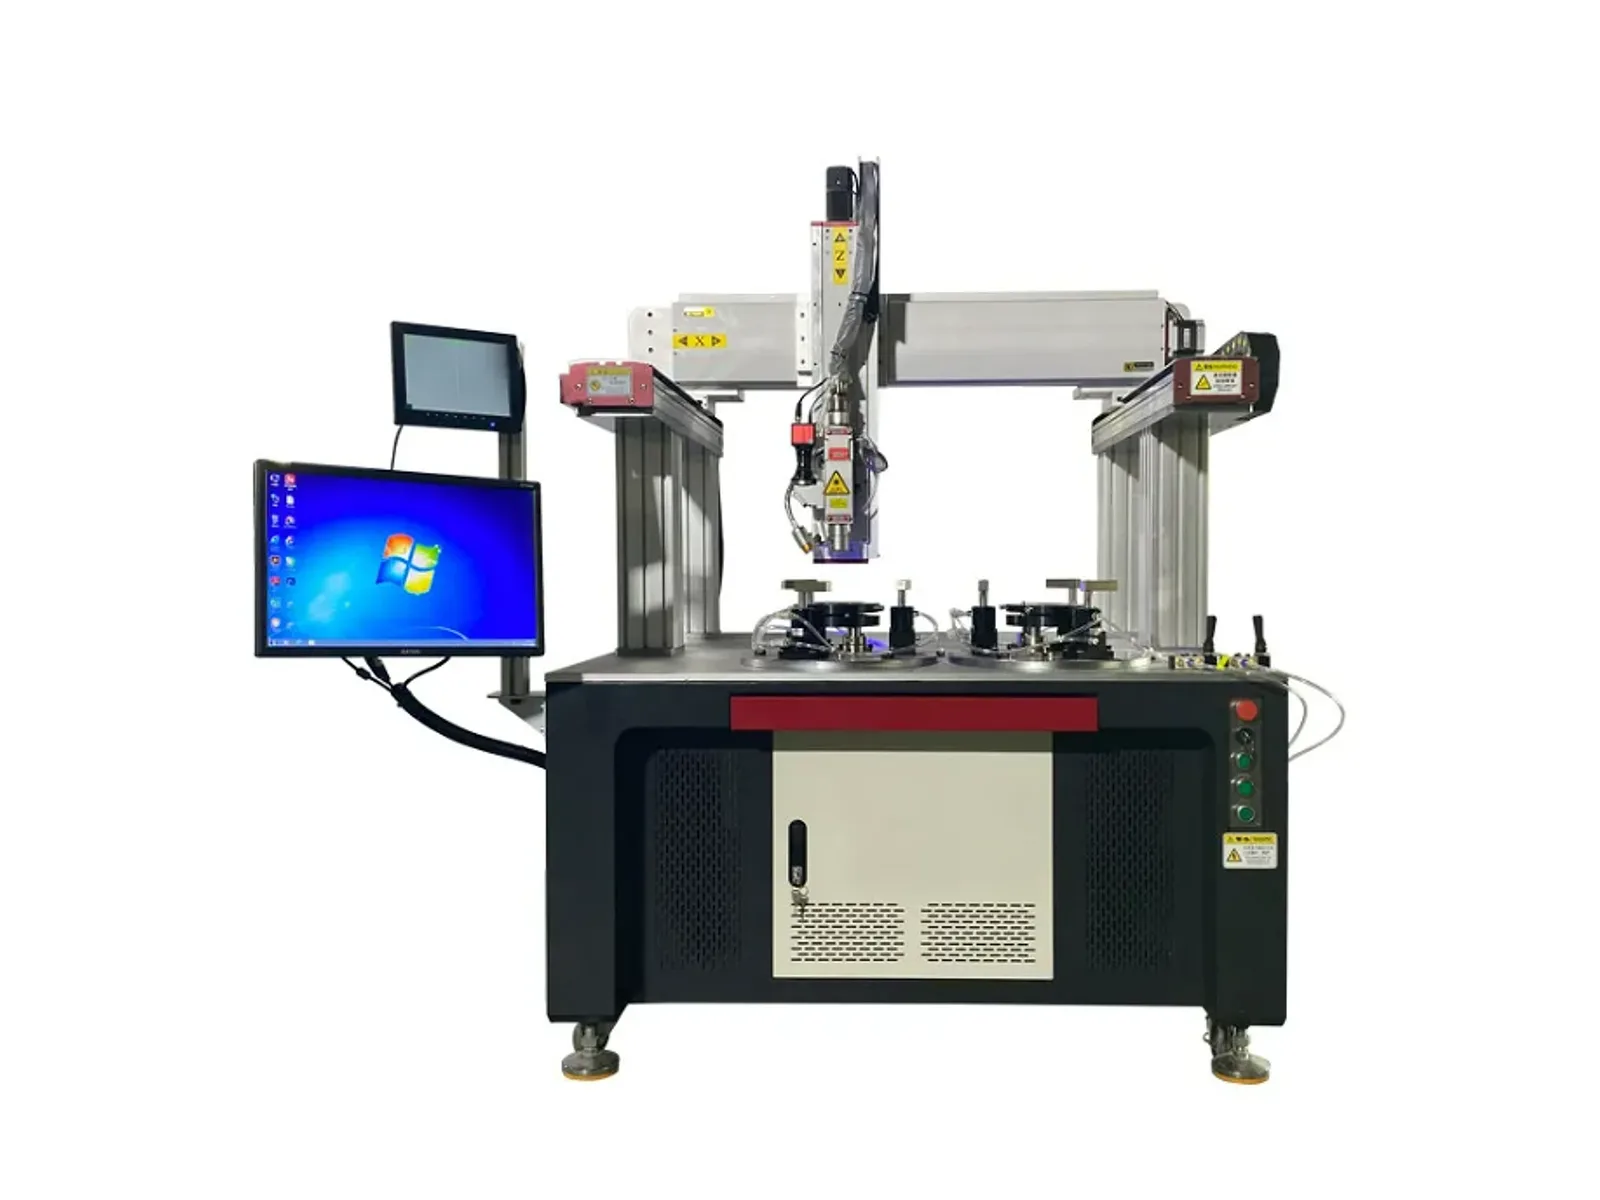
Sink Clamp Laser Welding Machine
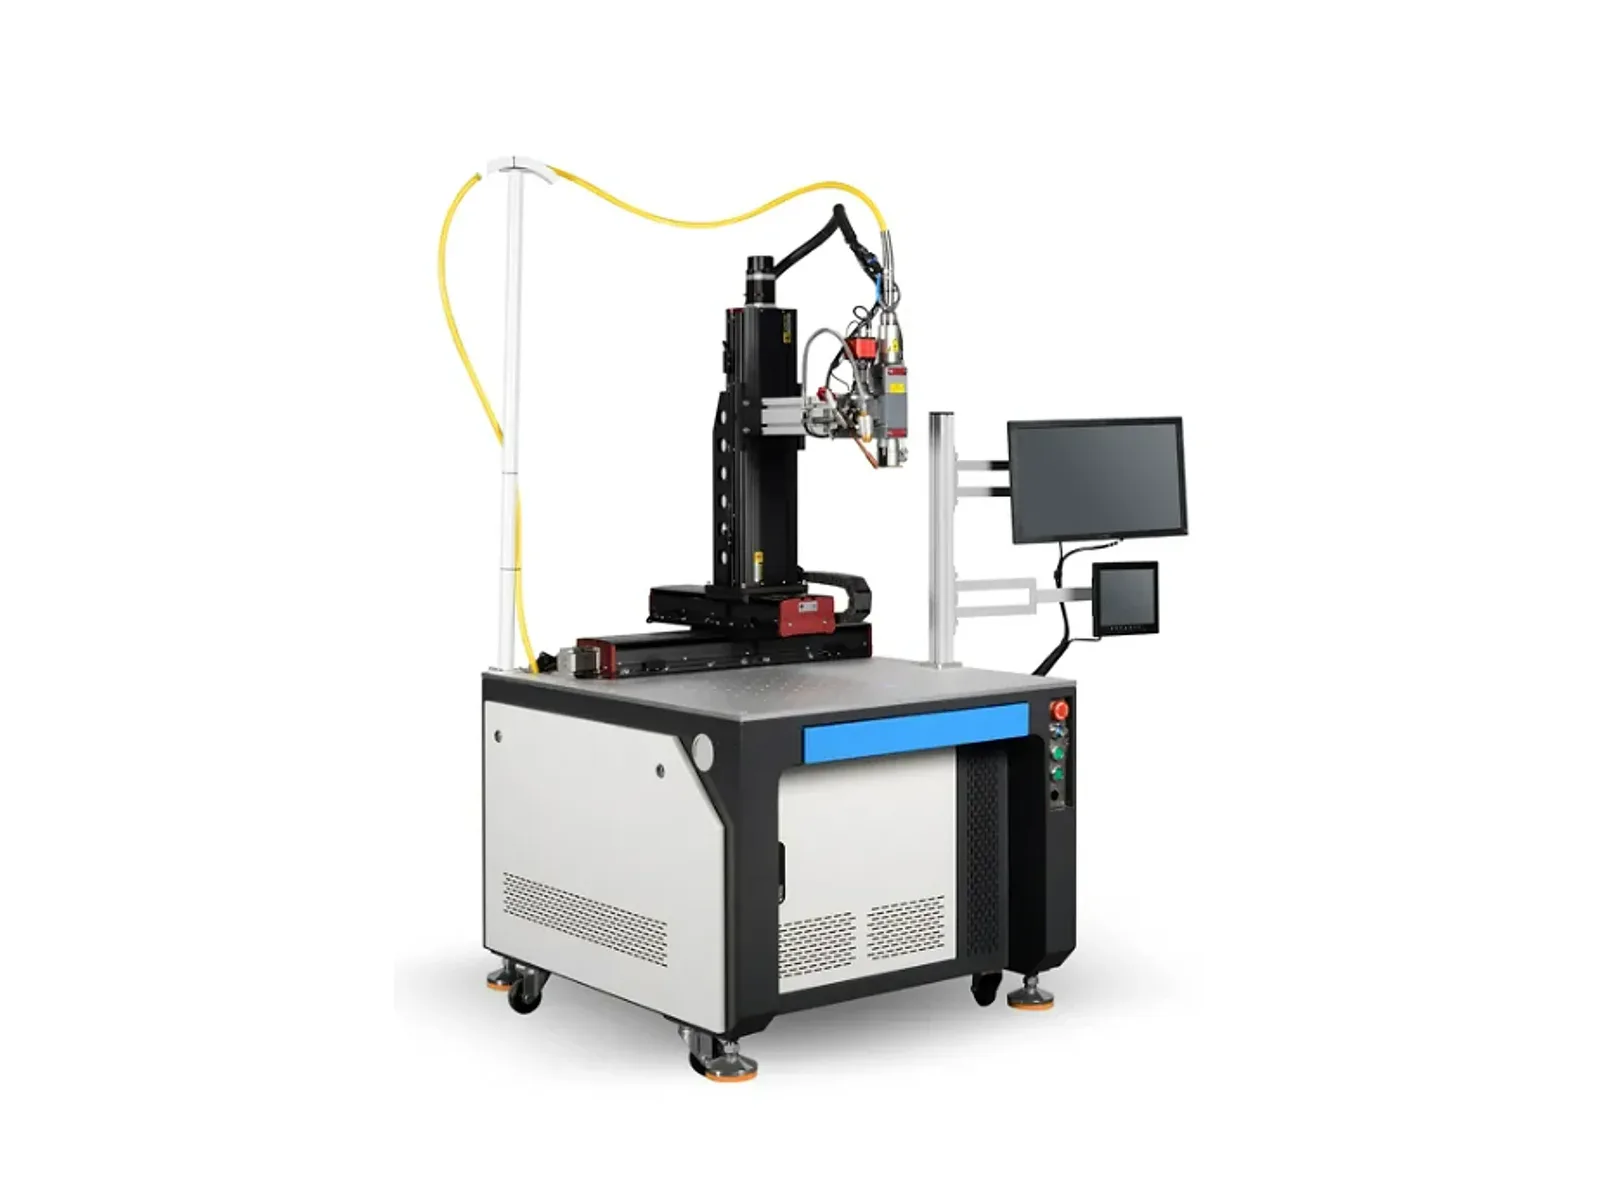
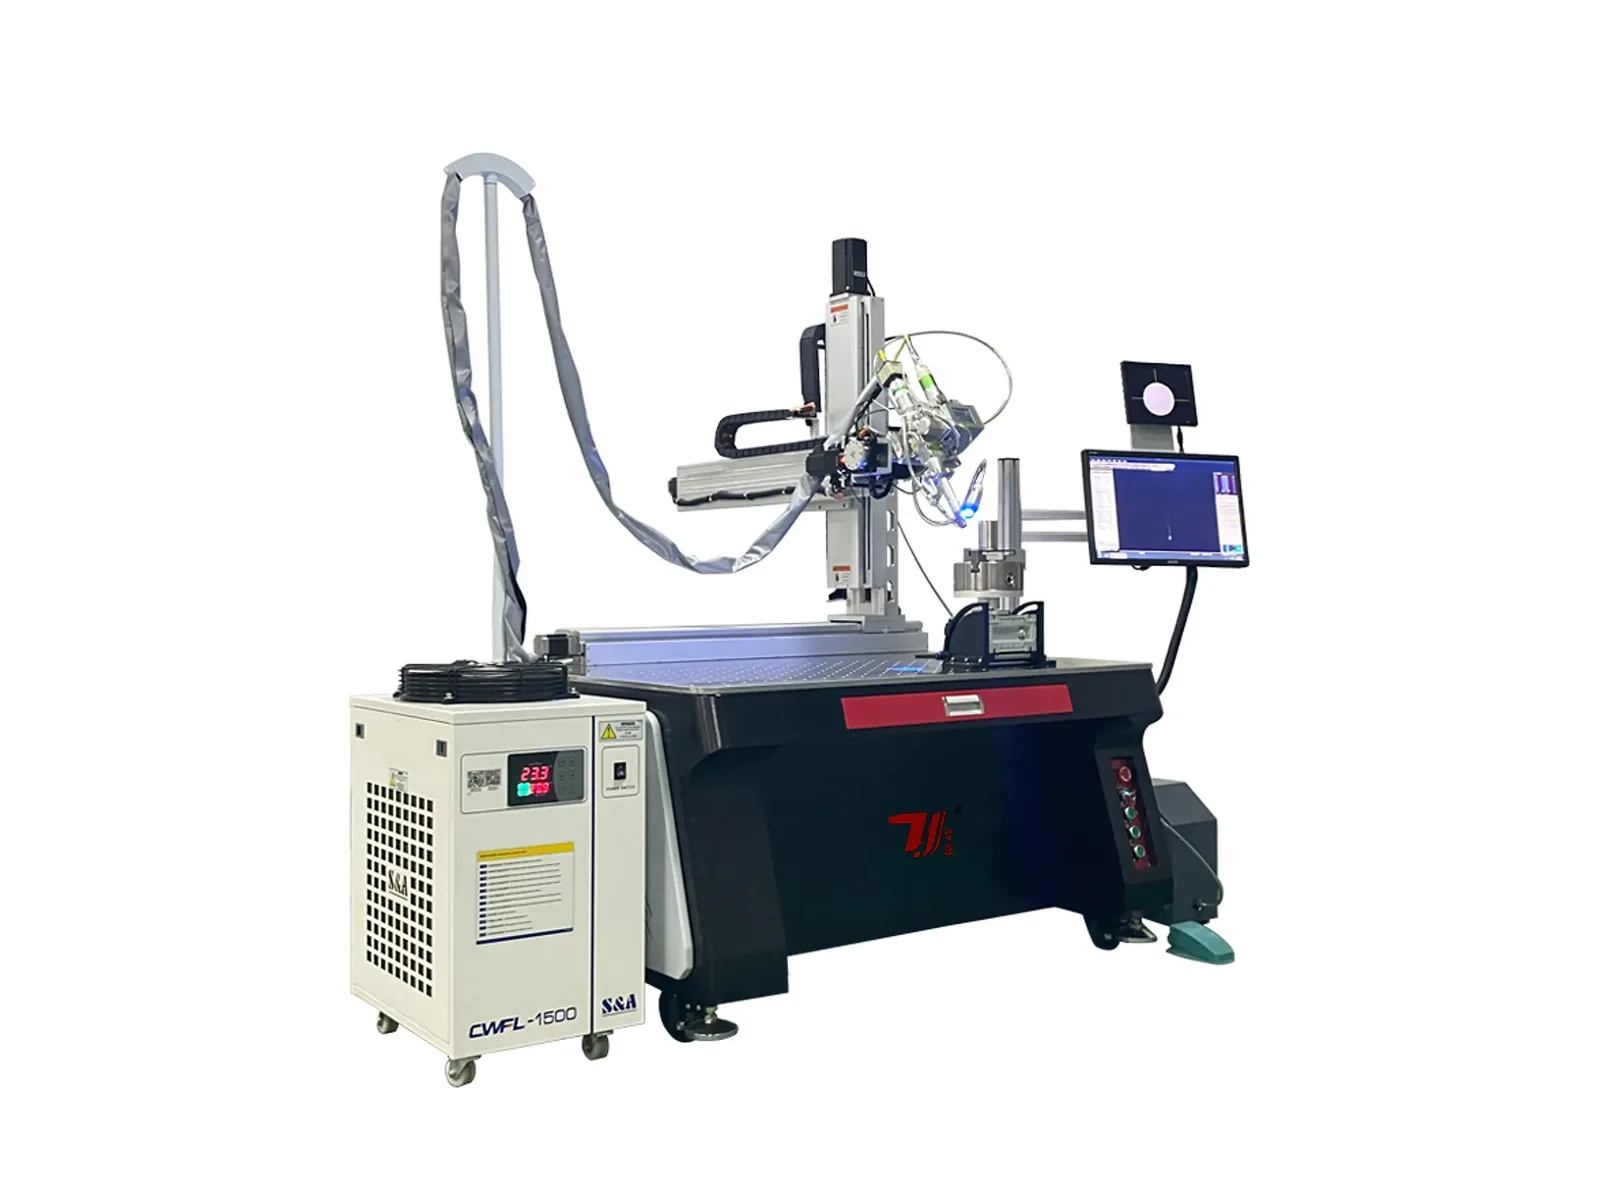
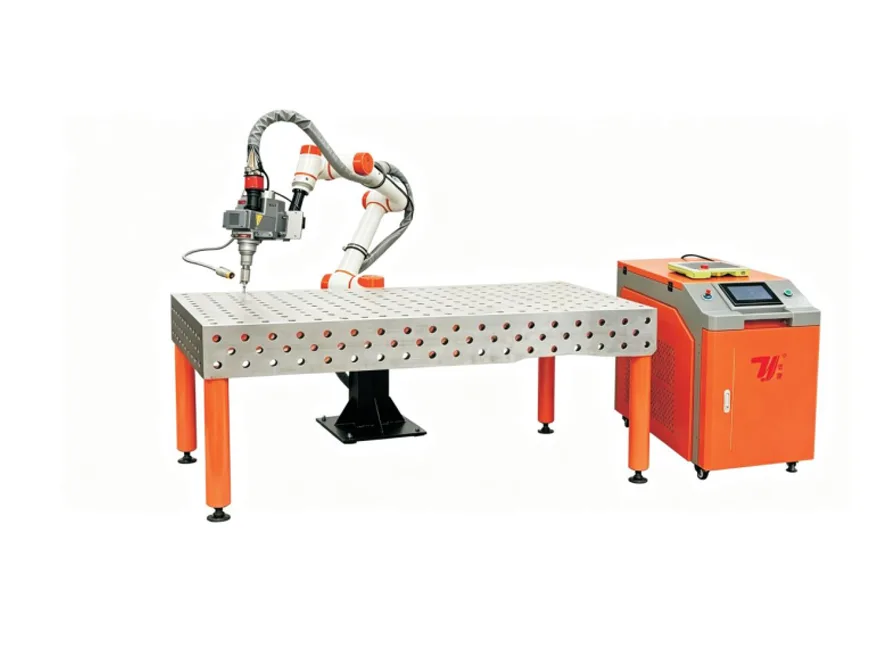
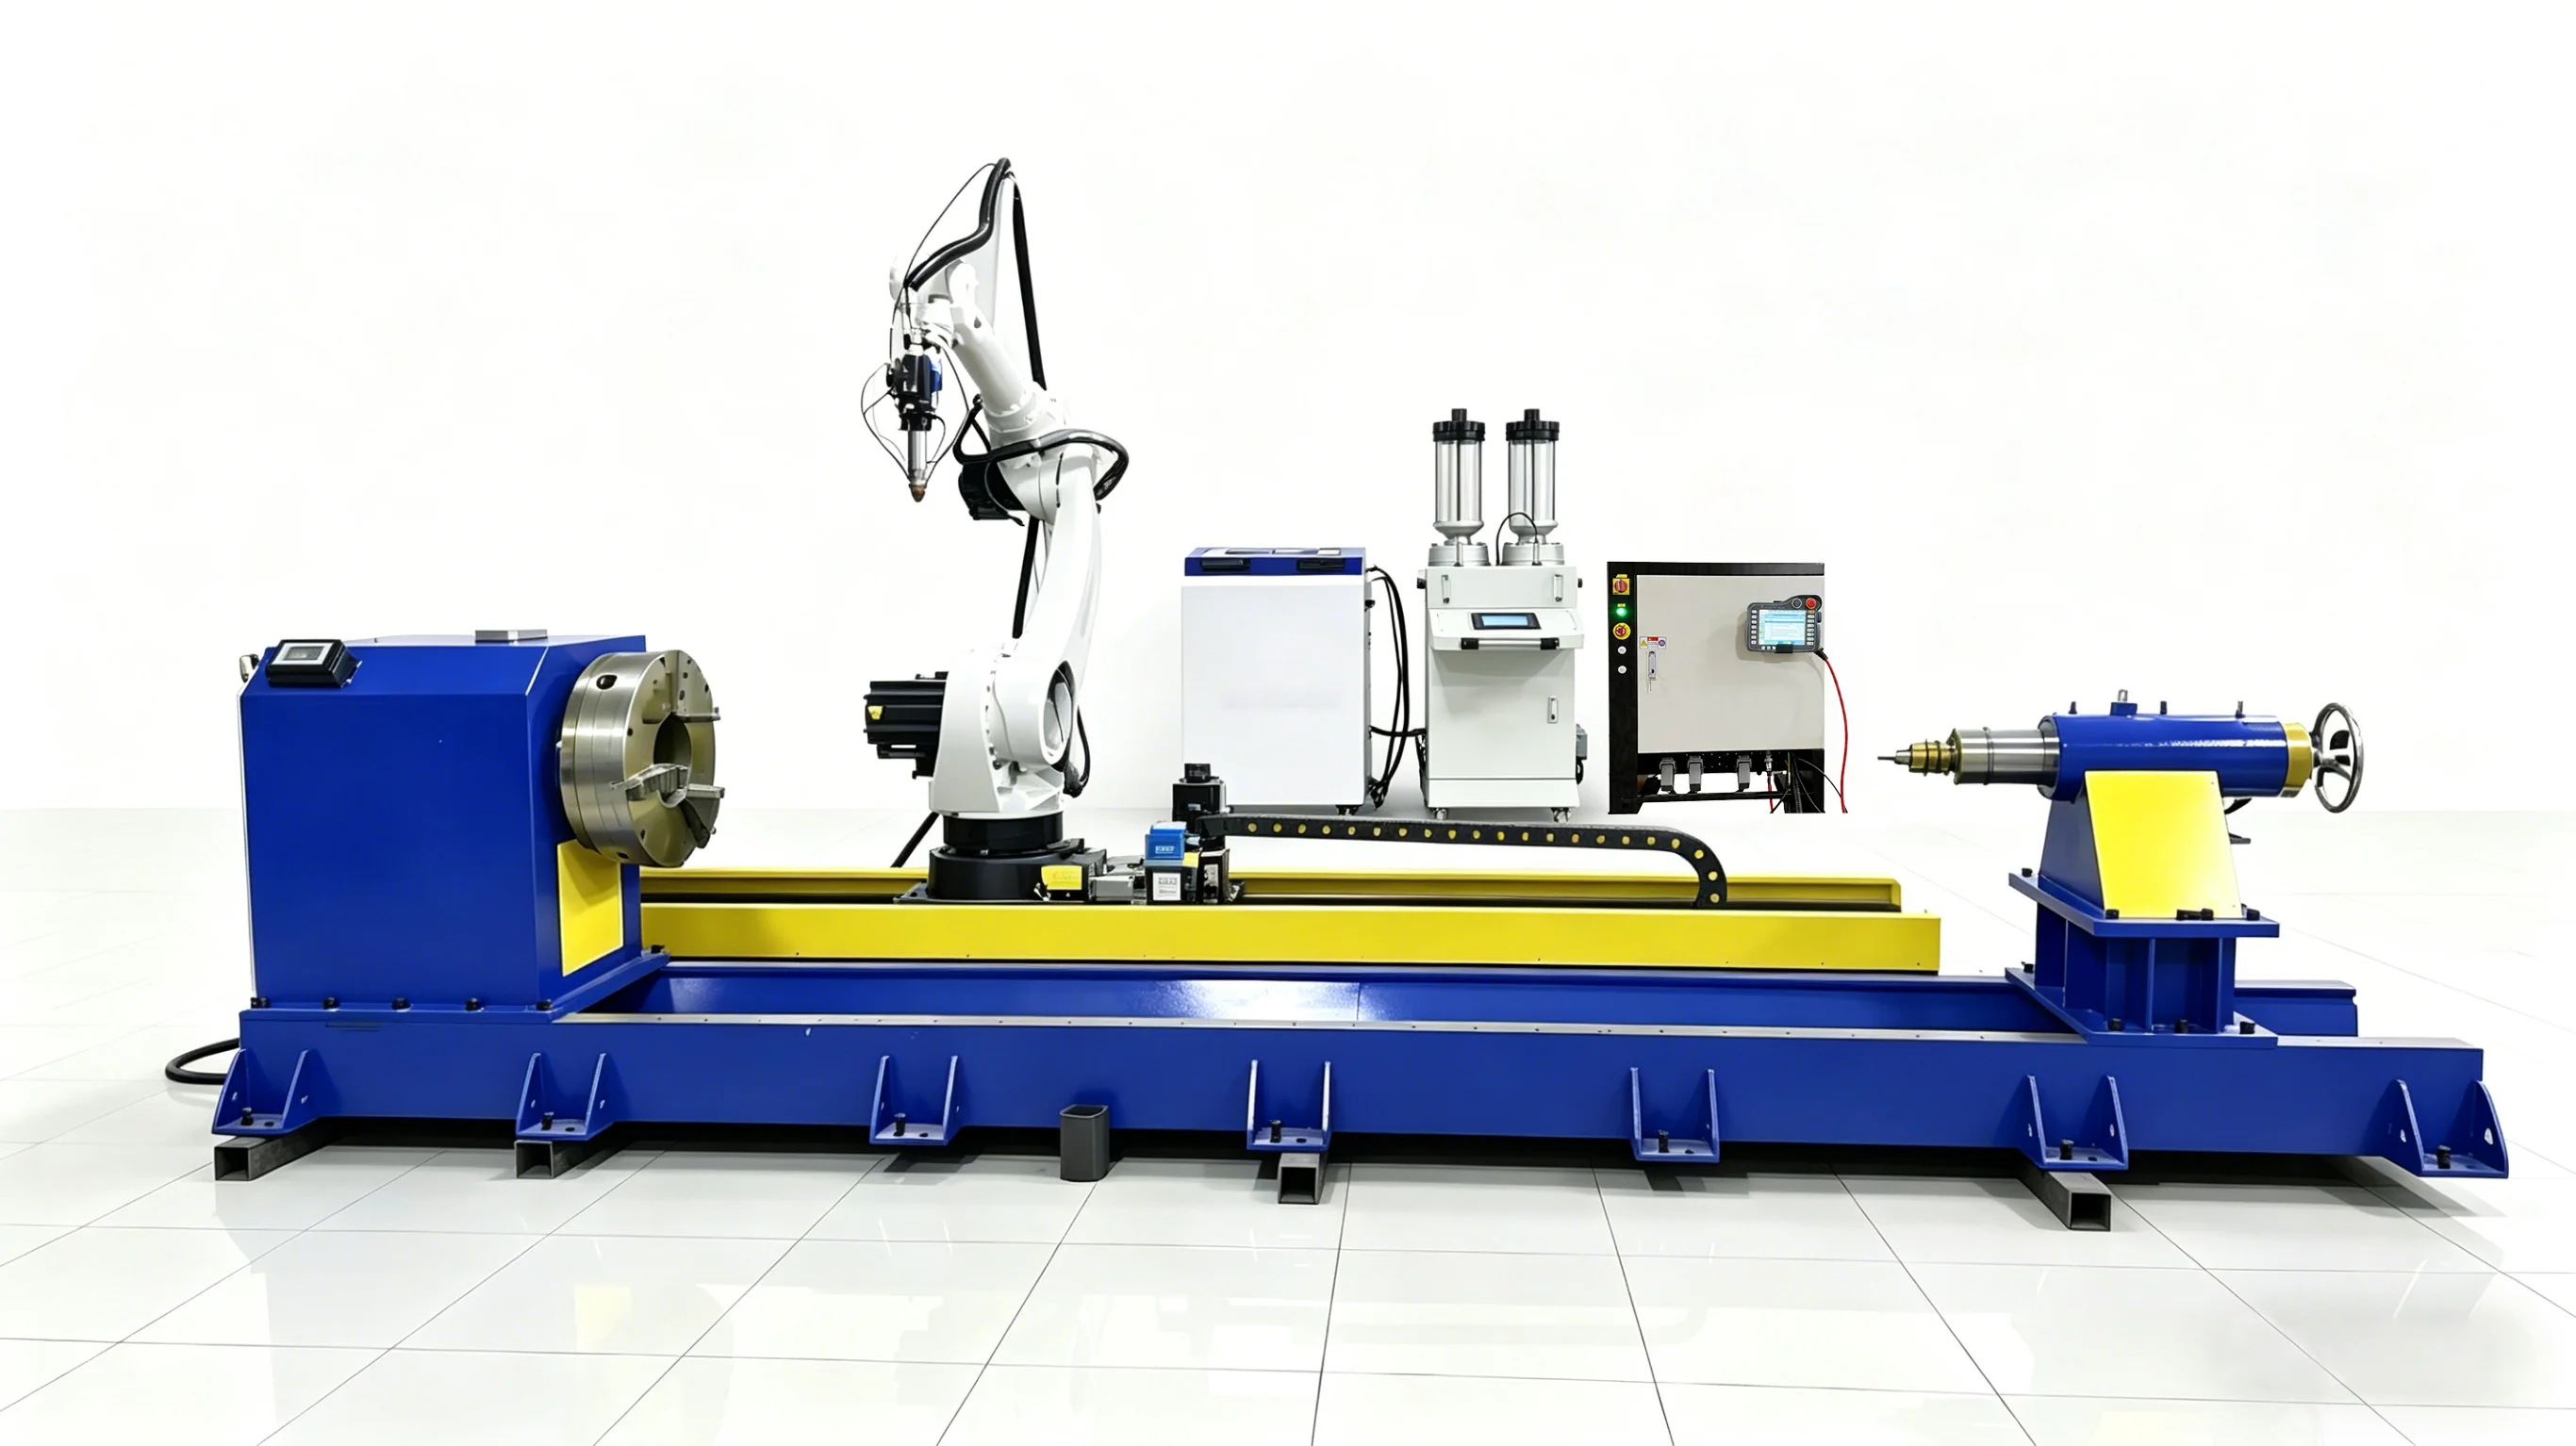
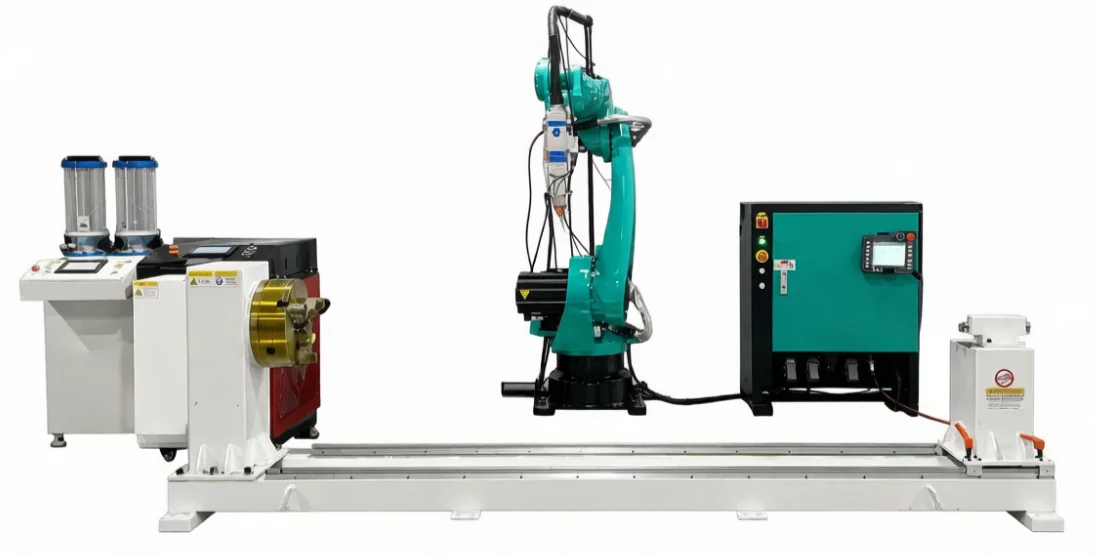
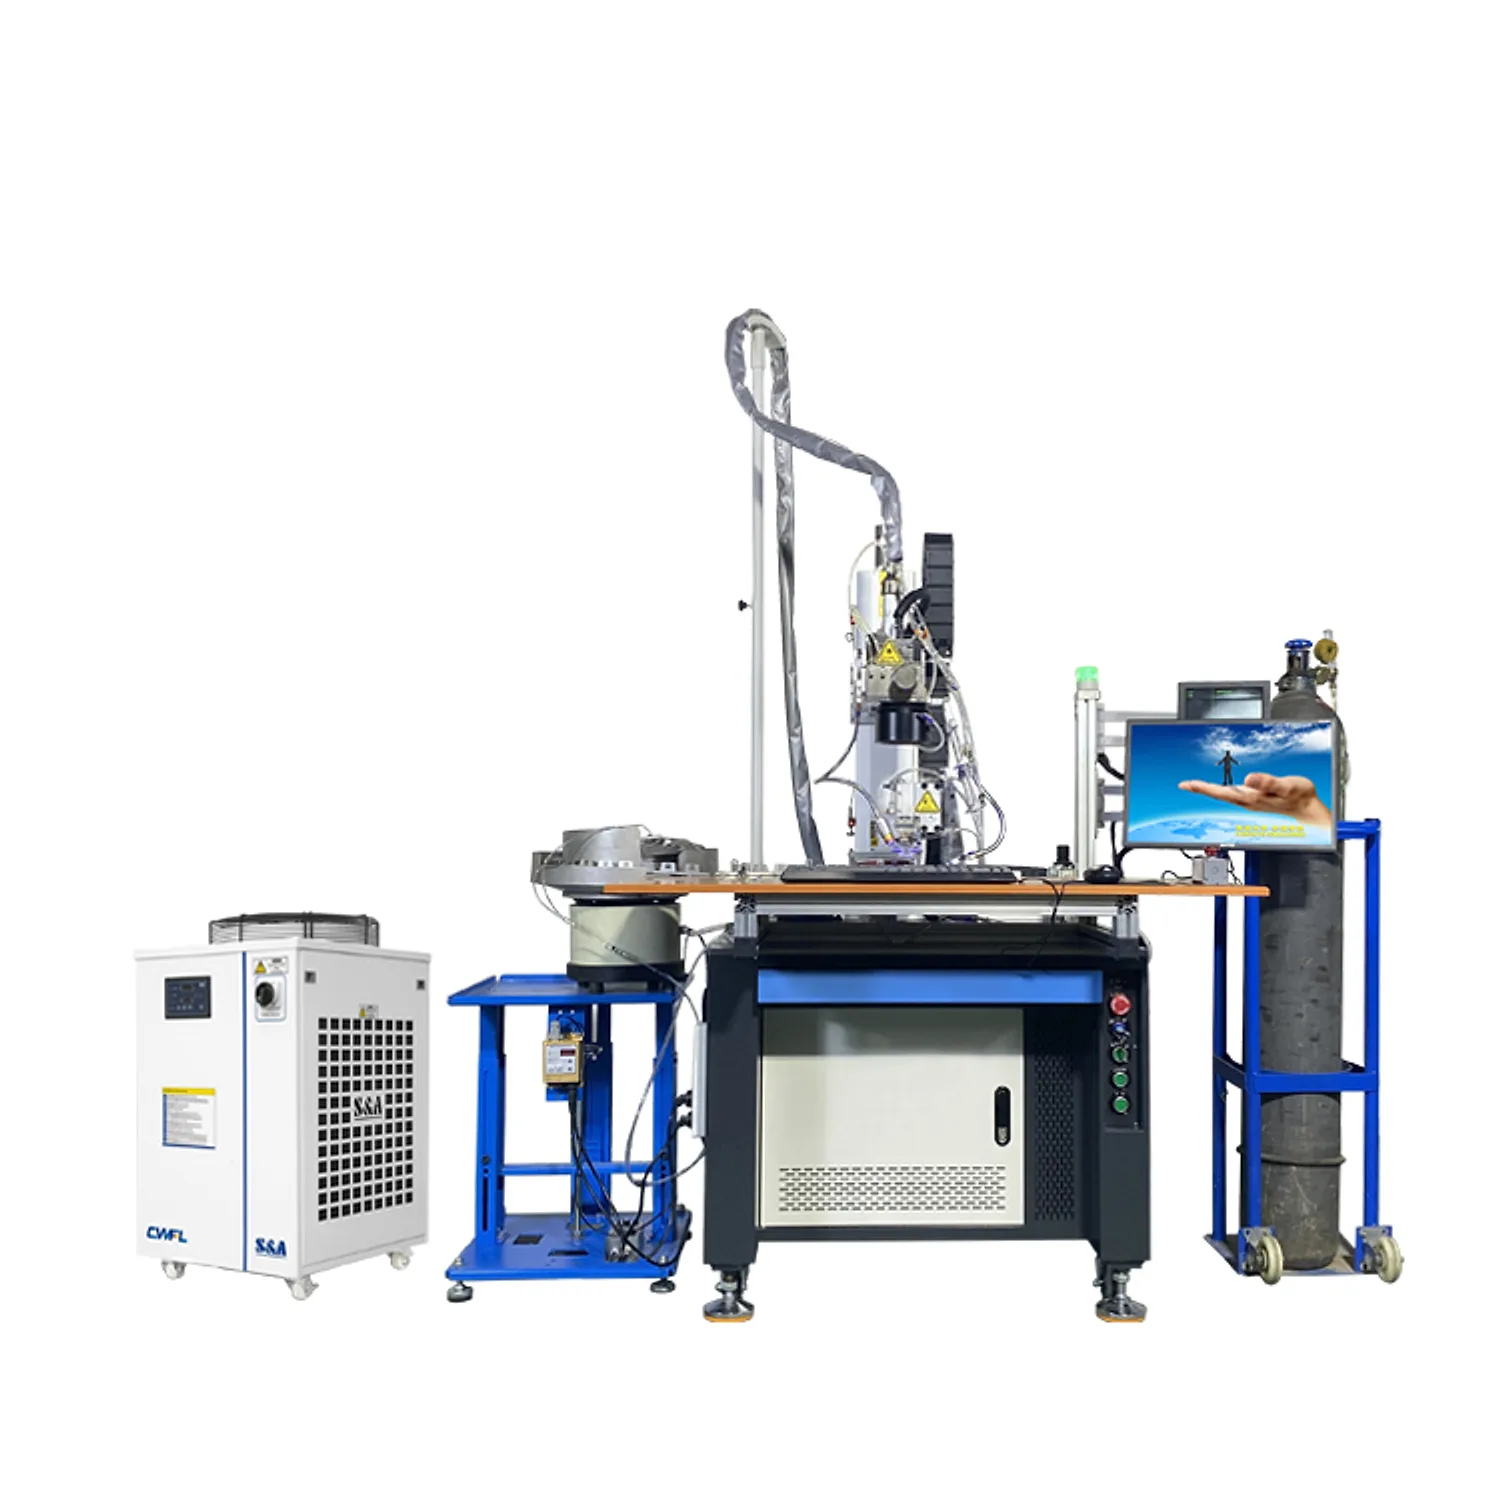
This automatic laser welding cell joins stainless-steel sink clamps, buckles and accessories using fixtures configured to the submitted sink model. Start with the accessory-to-sink joint and the variants you need to produce.
Specifications
Sink clamp welding system data
Laser and motion
- Laser power
- 1,500-6,000 W
- Welding speed
- 8-80 mm/s
- Servo positioning accuracy
- ±0.02 mm
- System type
- Dedicated automatic fixture-based welding cell
Workpiece and process
- Primary workpieces
- Stainless-steel sink clamps, buckles and accessories
- Fixture change
- Quick-change fixture support
- Variant handling
- Multiple sink models subject to fixture review
- Process objective
- Smooth seams with limited spatter and thermal deformation
Production integration
- Operating mode
- Automatic application-specific welding
- Production-line connection
- Supported
- Fixture package
- Configured to the submitted sink model
- Final configuration
- Confirmed after sample and cycle-time review
Hold the sink clamp securely through a repeatable weld cycle
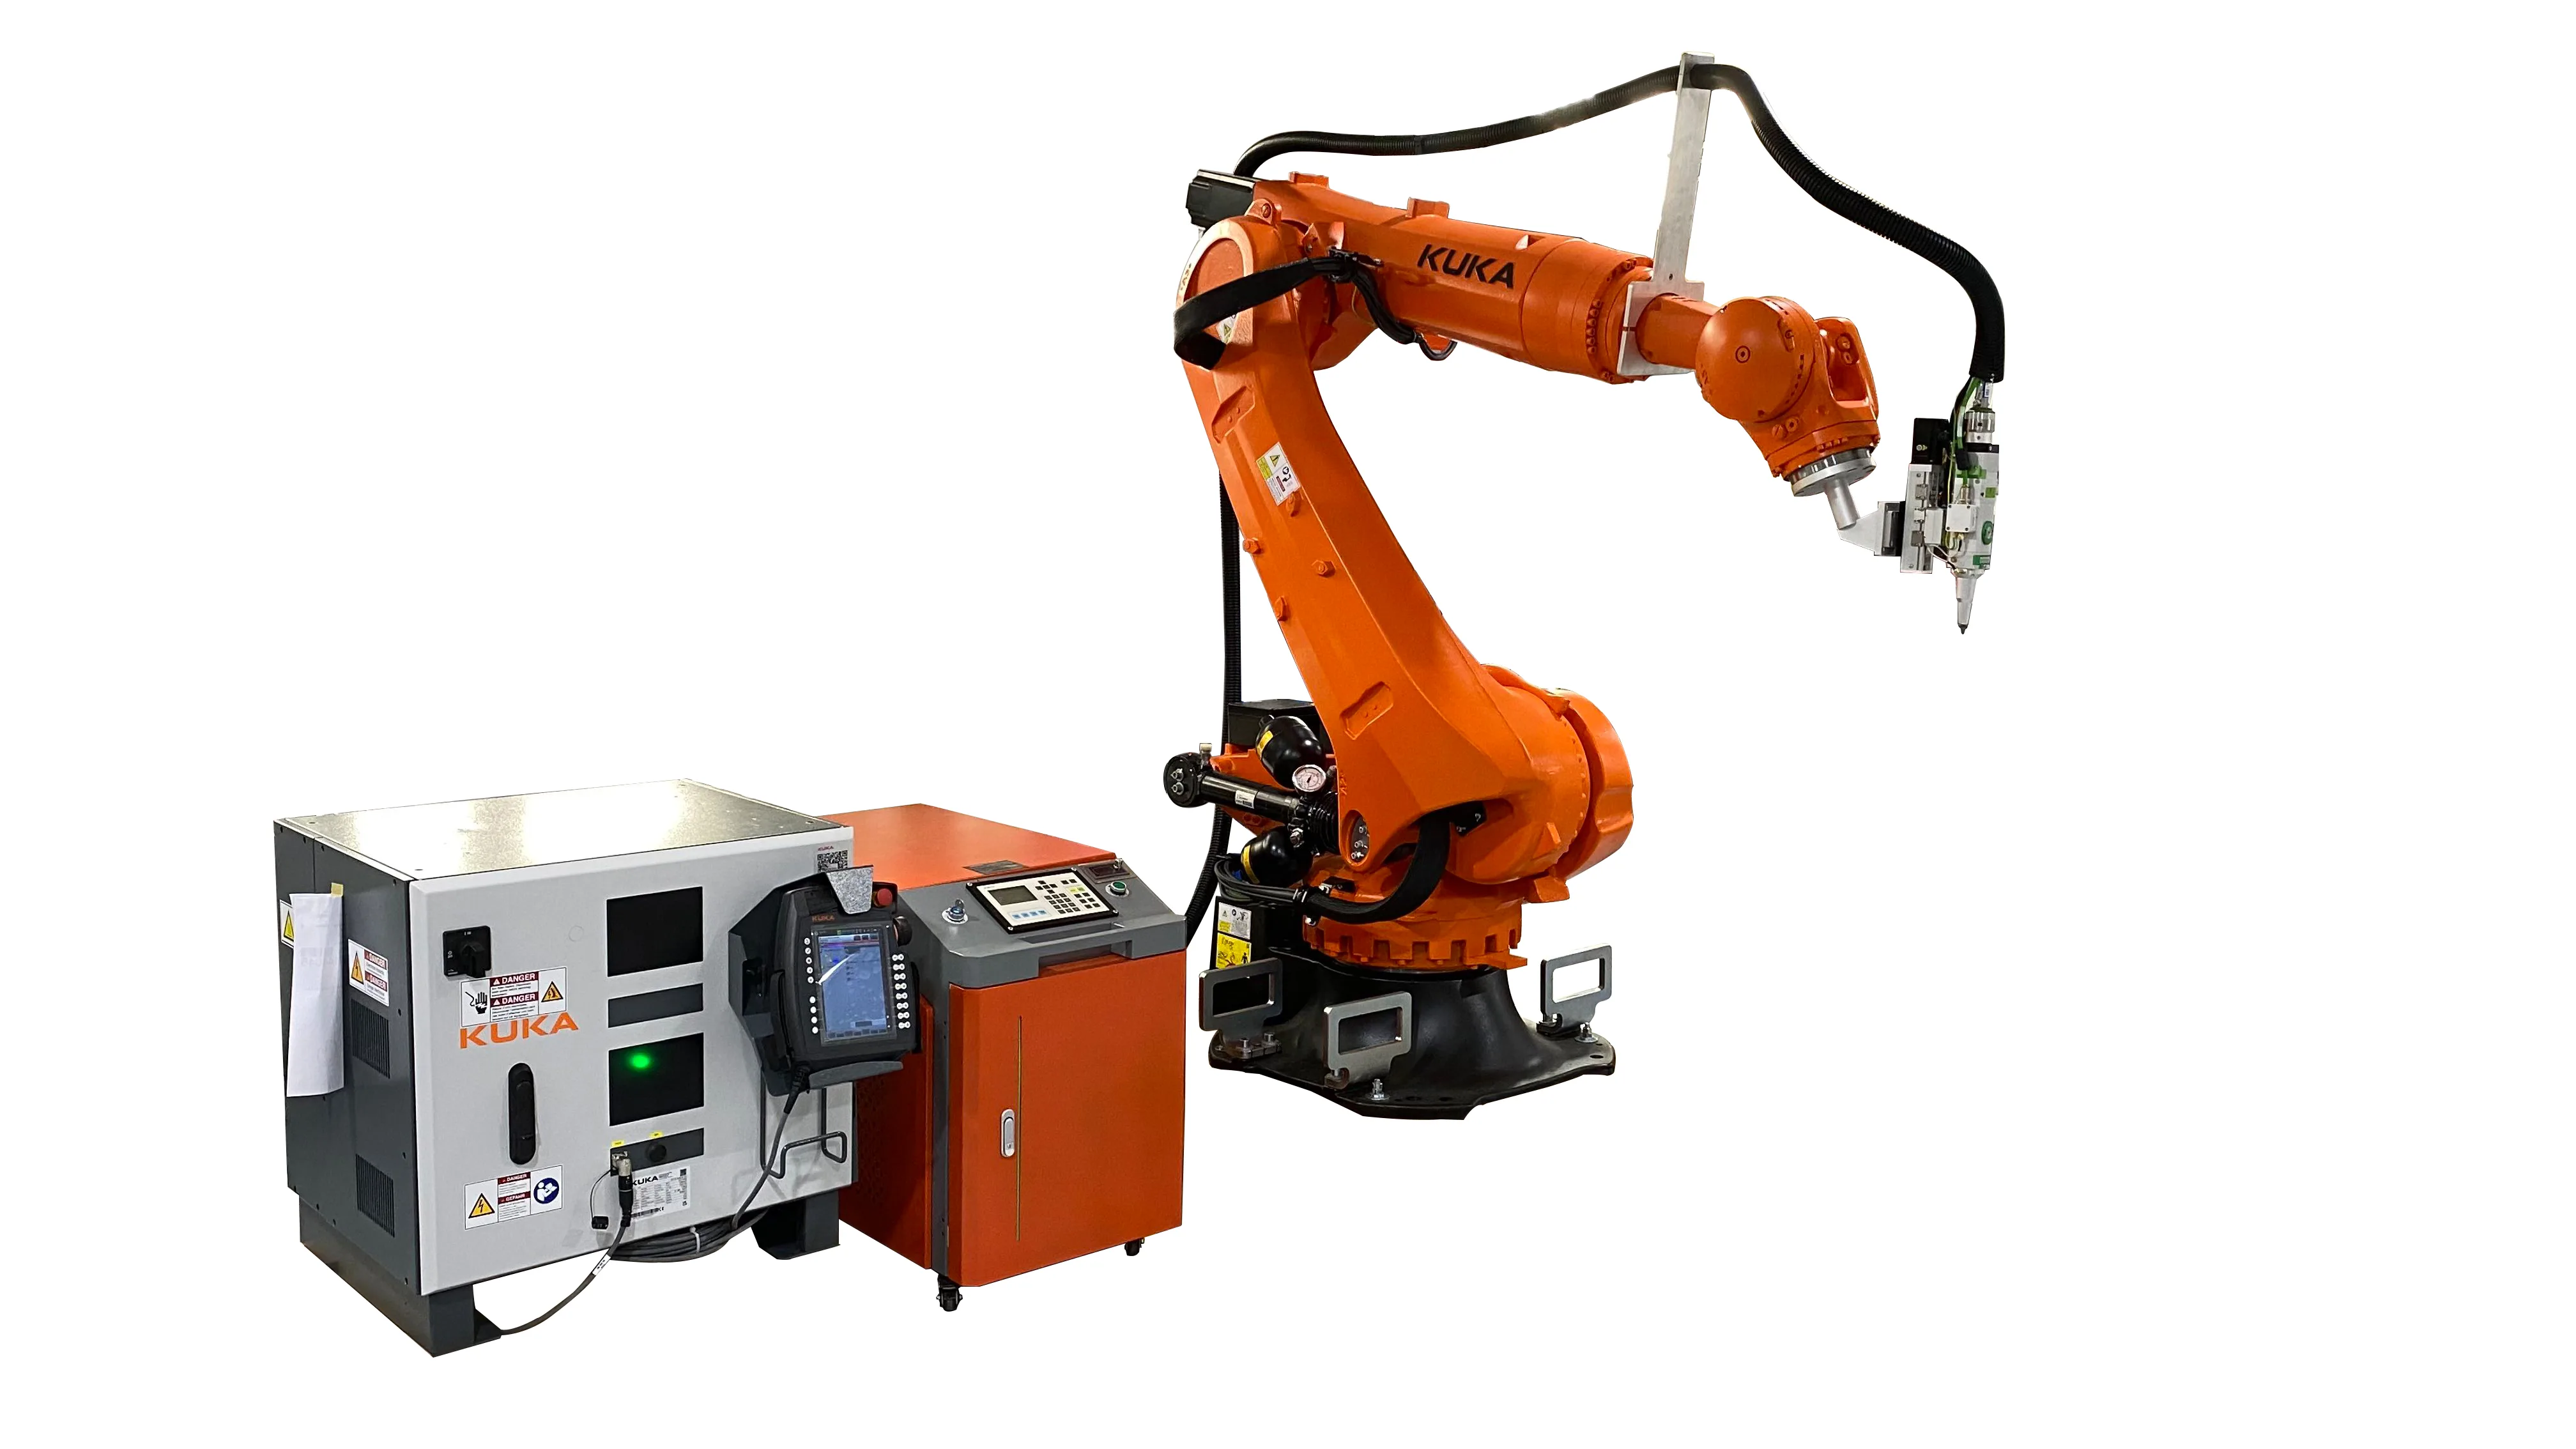
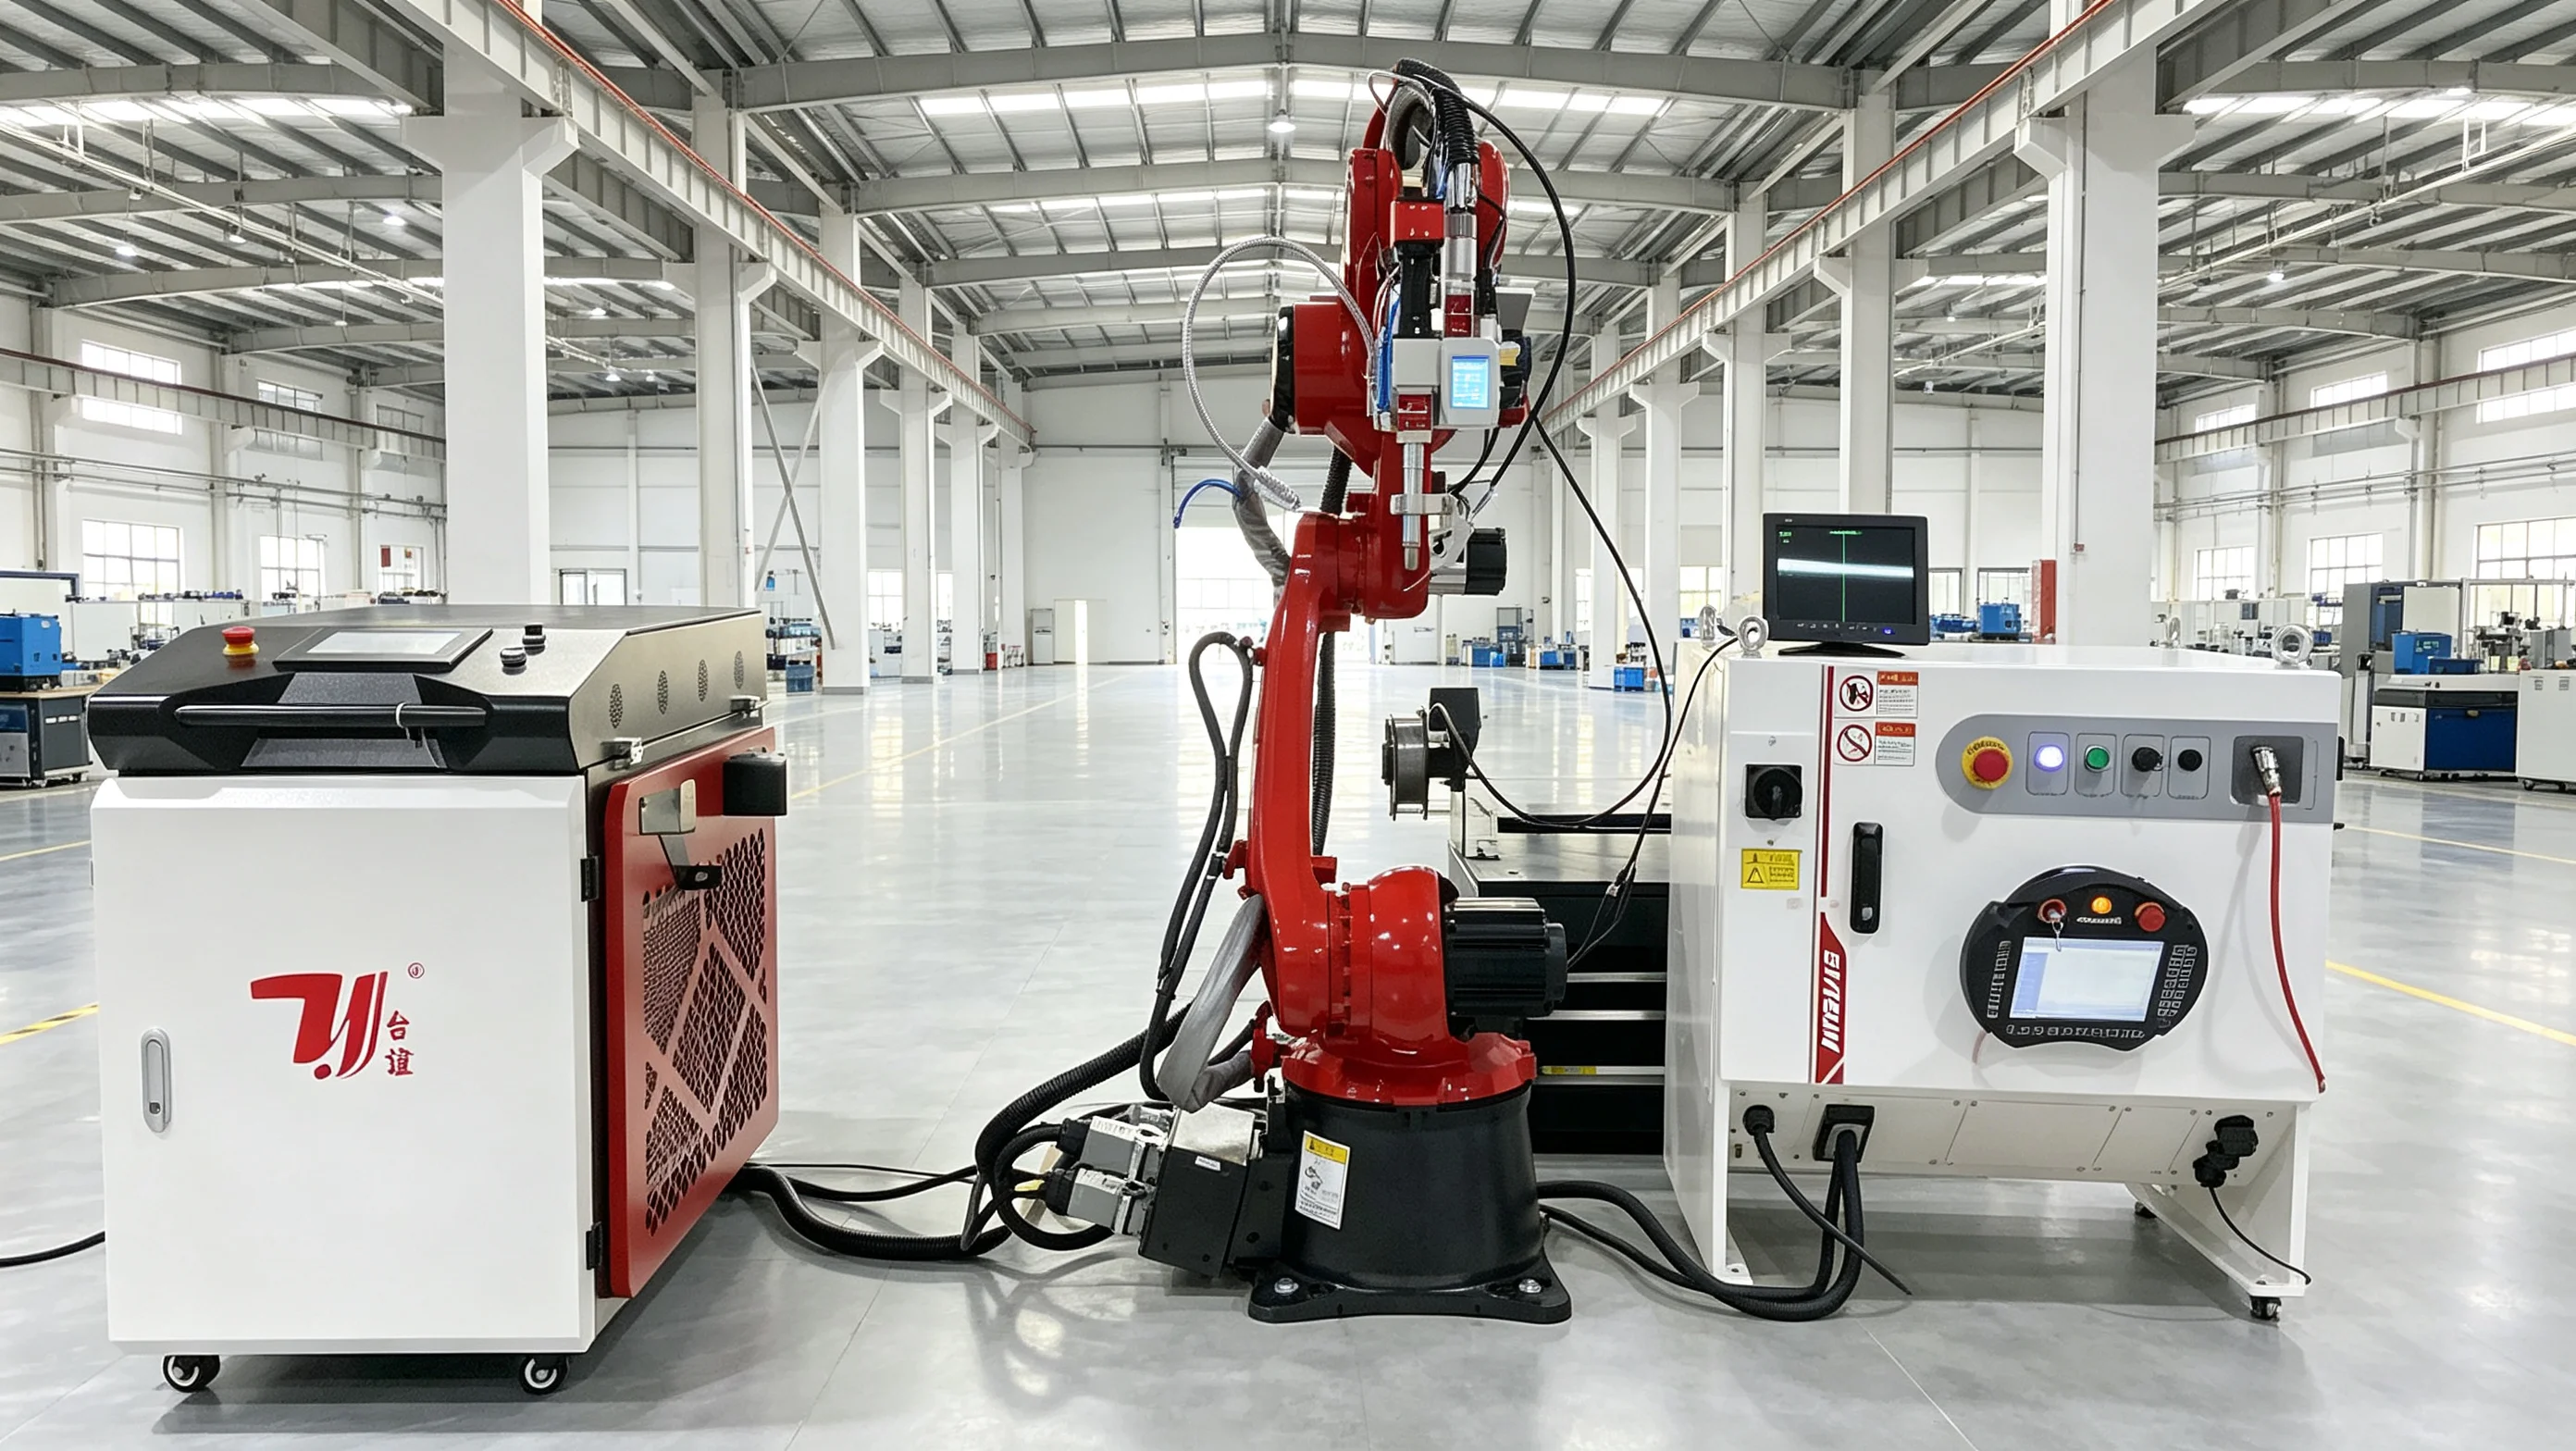
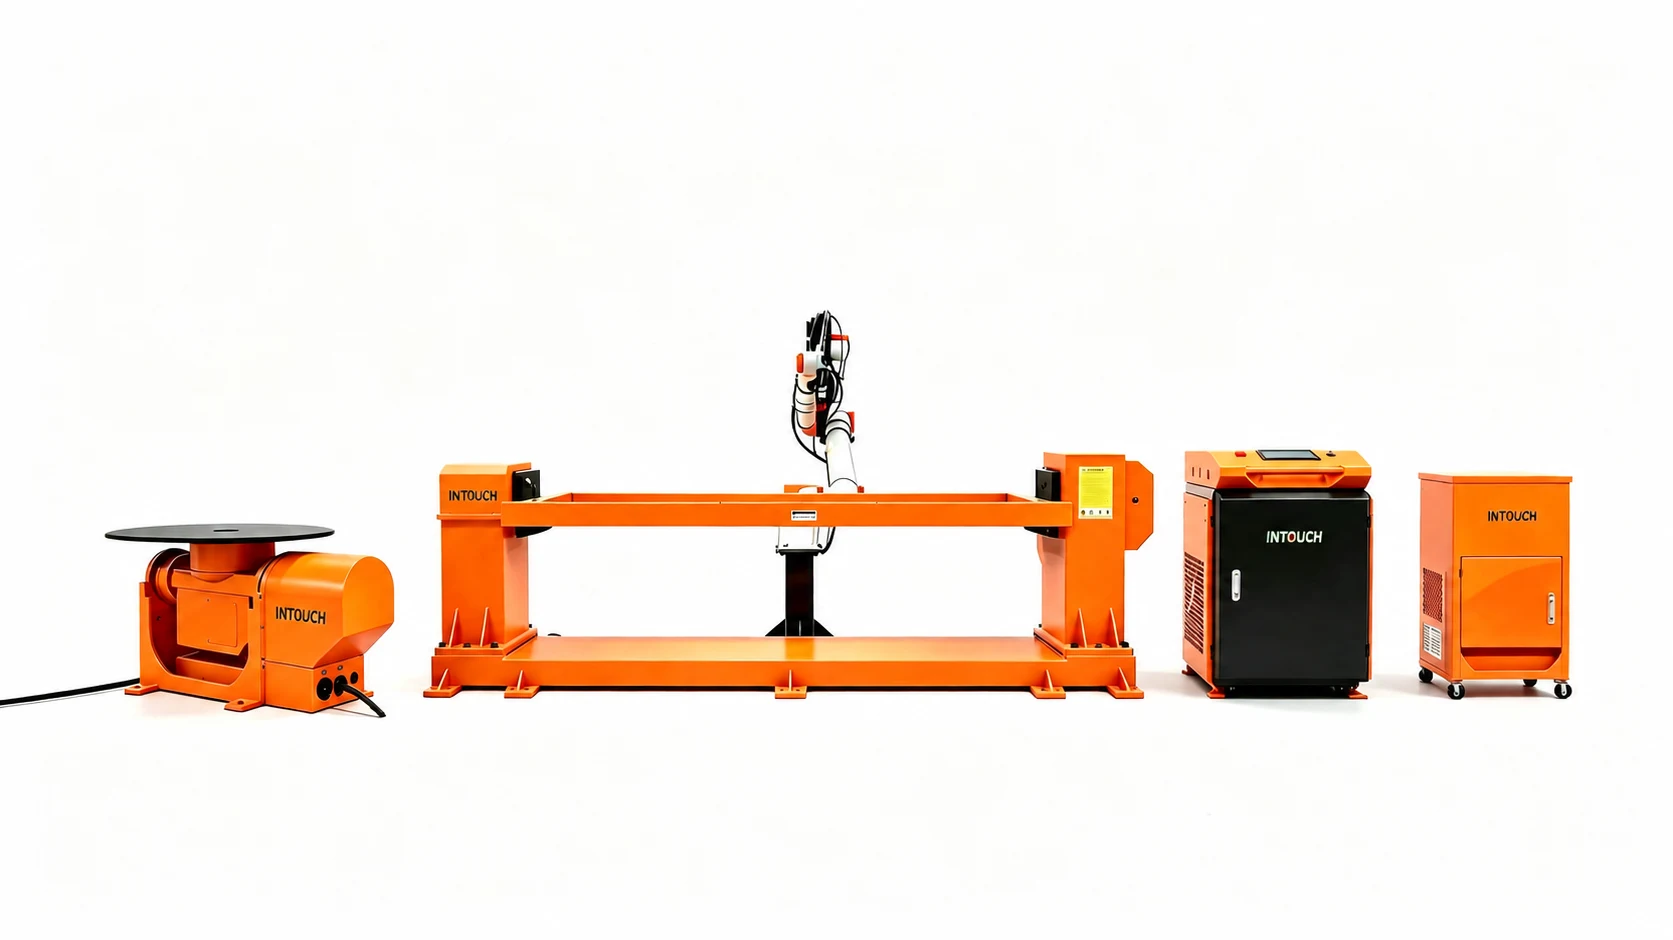
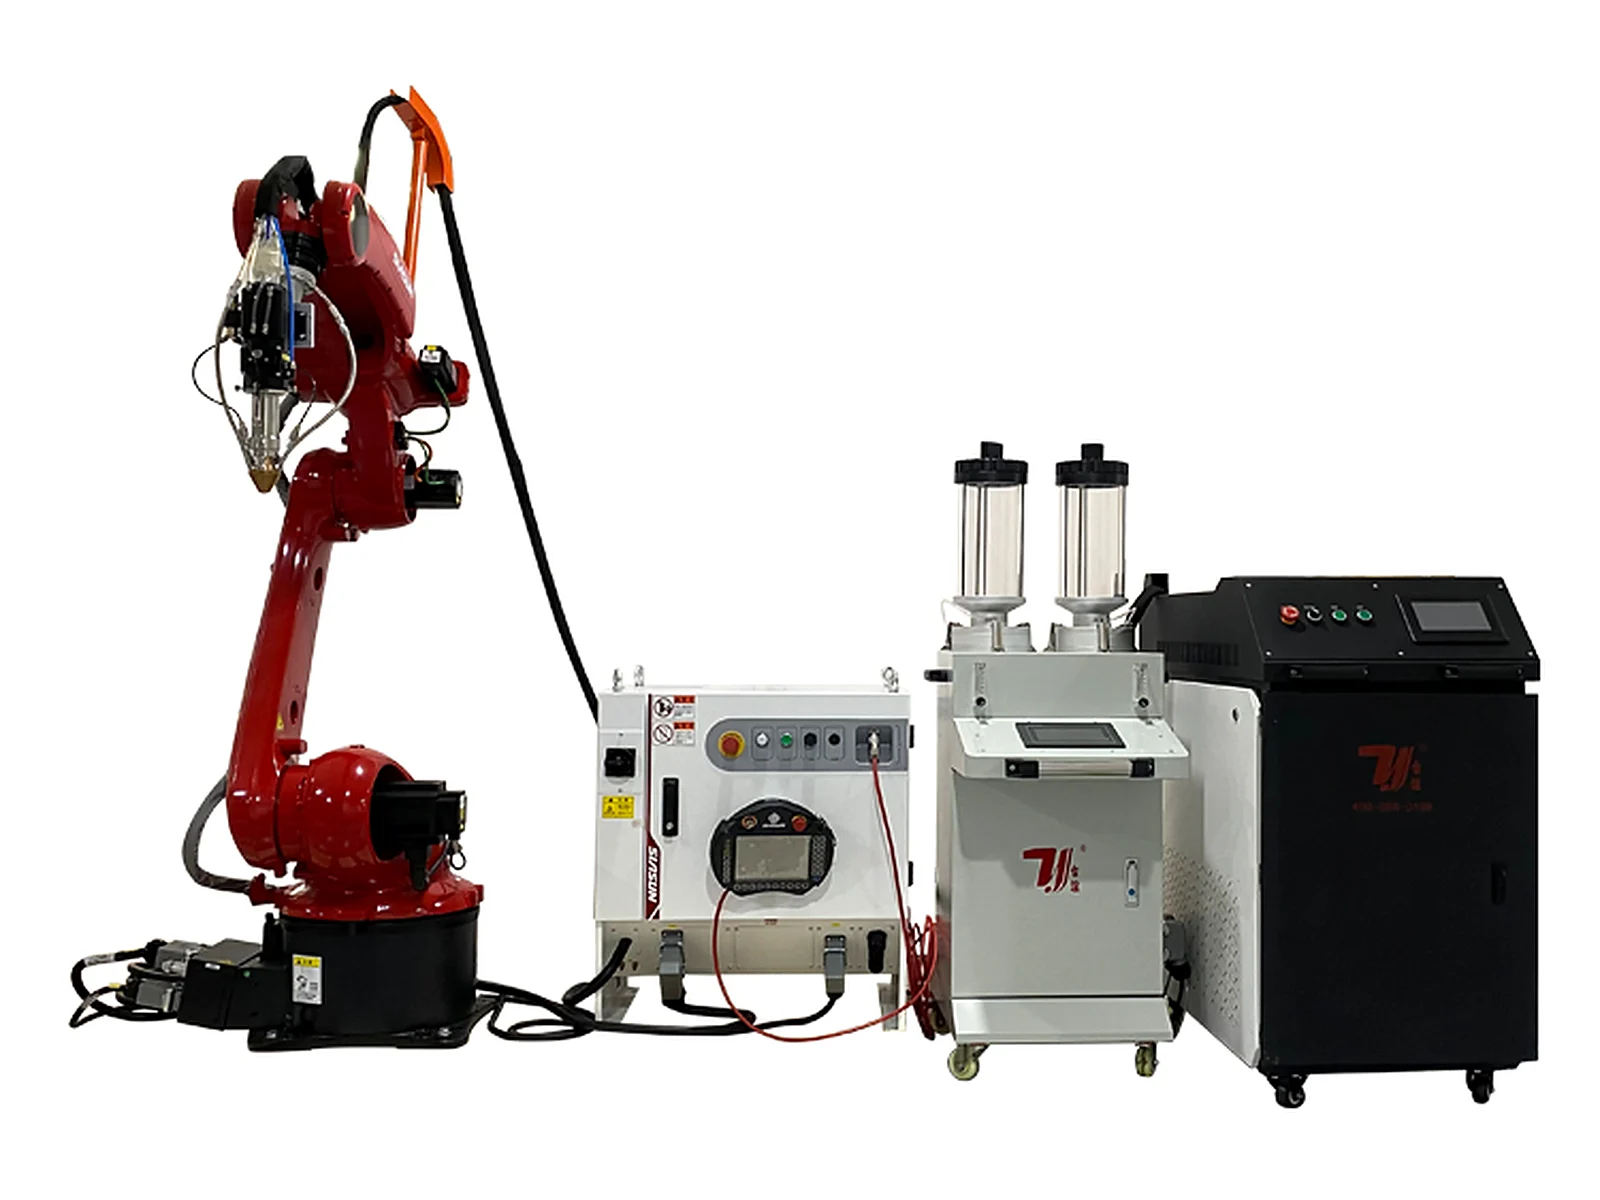
This is an application-configured cell rather than a fixed catalogue model. The fixture, laser source, weld path and automation interface are selected after the sink, clamp and production task are reviewed.
Dedicated sink-clamp fixture
The workholding layout is designed around the actual clamp or buckle geometry so the joint remains registered through the welding cycle.
Quick fixture change for variants
Quick-change fixture support allows multiple stainless-steel sink models to be reviewed within one application-specific production concept.
Controlled heat input
The supplied product table identifies smooth seams, limited spatter and reduced thermal deformation as process objectives. Final acceptance is established during sample development.
Prepared for line integration
A production-line connection can be included after loading, unloading, guarding and cycle-time boundaries are confirmed.
From application review to delivery
- 01
Machine-bed welding
- 02
Beam preparation
- 03
Heat treatment
- 04
Precision machining
- 05
Pre-assembly inspection
- 06
Machine assembly
- 07
Testing, debugging and acceptance
- 08
Delivery
Application scope for sink-clamp and accessory welding
Suitability depends on the stainless-steel grade, clamp geometry, fit-up, weld depth and target cycle time. Submit the actual sink and joint data before fixing the process route.
Compare the next automation path
Multi-station kettle-spout welding
Multi-station configurations for repeat kettle-spout, body and bottom seams.
Five-axis linked systemFive-axis automatic welding
Configurable motion for three-dimensional curved surfaces and special-shaped workpieces.
Application systemsAutomatic welding range
Compare gantry, multi-axis and workpiece-specific automatic welding systems.
Related industry solutions
Explore the applications and laser processes connected to this equipment.
View all industry solutions
Define the clamp joint before selecting the cell
Locate the accessory and the weld
Provide a drawing showing the clamp or buckle against the sink, including the contact surfaces, joint dimensions and access around the seam. These details establish what the fixture must locate and where the welding head needs clearance.
Plan the sink variants together
Quick-change fixture support is available for reviewed sink models. List each model and the differences in clamp position, shape and sink dimensions so the fixture sets and changeover work can be defined before quotation.
Agree on appearance and production scope
State the required seam appearance, permitted distortion and inspection method alongside the cycle target. Loading, unloading and line connection need a defined scope; automatic welding alone does not establish the complete production sequence.
Machine selection questions
Is this machine for welding the whole sink body?
The cell described here is intended for sink clamps, buckles and accessories. A basin-body or panel seam requires a separate joint and machine review; it should not be assumed to use the same fixture or process.
Can one cell handle different sink models?
Multiple sink models can be reviewed with quick-change fixture sets. Compatibility depends on the sink envelope, accessory location and access to each joint; submit the full variant list when requesting a configuration.
Does the positioning specification define finished weld quality?
The listed servo positioning accuracy describes machine motion. Seam appearance, distortion and joint acceptance must be agreed for the actual material, fit-up and inspection method.
Can the cell connect to an assembly line?
Production-line connection is supported after project review. Specify who supplies loading, unloading and the surrounding line equipment so the interfaces and operating sequence can be included in the proposal.
What is needed for a sink-clamp welding quote?
Send the sink and accessory drawings or samples, stainless-steel grades, joint dimensions, model variants, cycle target and appearance or inspection requirements. This gives TAIYI a basis for reviewing the fixture and process package.
Request a quote
Tell us the part. We will tell you the machine.
Configuration and quotation are prepared after the sink model, clamp geometry, material, joint and production target are reviewed.
- Phone+86 153 6281 4831
- Emailsales02@taiyilaser.com
- WhatsApp+86 153 6281 4831